Tissue Converting Line Solutions for Enhanced Production Efficiency
2026-10-12
Every minute a tissue converting line runs below its potential, margins quietly erode. Operators know the frustration: a line that should be flying instead crawls through roll changes, splices, and jams. DAXIN takes a different approach—not by adding more machinery, but by rethinking how each stage of converting works together. The result isn't just a faster line; it's a line that finally delivers on the efficiency you were promised. Here's what that looks like in practice.
The Real Reason Lines Slow Down at High Speed
When a signal travels down a wire, it doesn't just move along the metal surface. The electric and magnetic fields extend into the surrounding insulation and even into nearby conductors. At low speeds, these fields have time to settle, and the line behaves almost like a simple resistor. But as the frequency climbs, the changing fields start to interact more strongly with the material around the wire. This is where things get interesting: the insulation begins to absorb energy, and the wire's own resistance rises because current gets pushed toward the outer skin of the conductor. The result is that the signal loses more power per meter than you'd expect from a DC measurement.
There's another hidden factor that often gets overlooked: the dielectric material itself. Most insulators are not perfectly uniform, and their polarization can't keep up with very fast voltage changes. This lag creates a kind of internal friction, turning some of the signal energy into heat. At the same time, the geometry of the line starts to matter more. If there are bends, vias, or nearby ground planes, the electromagnetic fields can't spread out evenly. That uneven distribution raises the effective impedance locally, which causes reflections. Those reflected waves bounce back and forth, interfering with the original signal and making the overall transmission look slower and more lossy.
Perhaps the least intuitive part is that the speed of the signal itself doesn't change—what changes is how long it takes for the receiver to get a clean, usable voltage level. A digital edge is made of many frequency components. The higher-frequency parts get attenuated and delayed more than the lower ones, so the sharp edge becomes smeared out. The receiver then has to wait longer for the voltage to cross its threshold. That waiting time is what we perceive as the line slowing down at high speed. It's not the electrons moving slower; it's the shape of the waveform collapsing under the weight of physics that was always there, just waiting to be noticed.
How Web Tension Quietly Sabotages Output
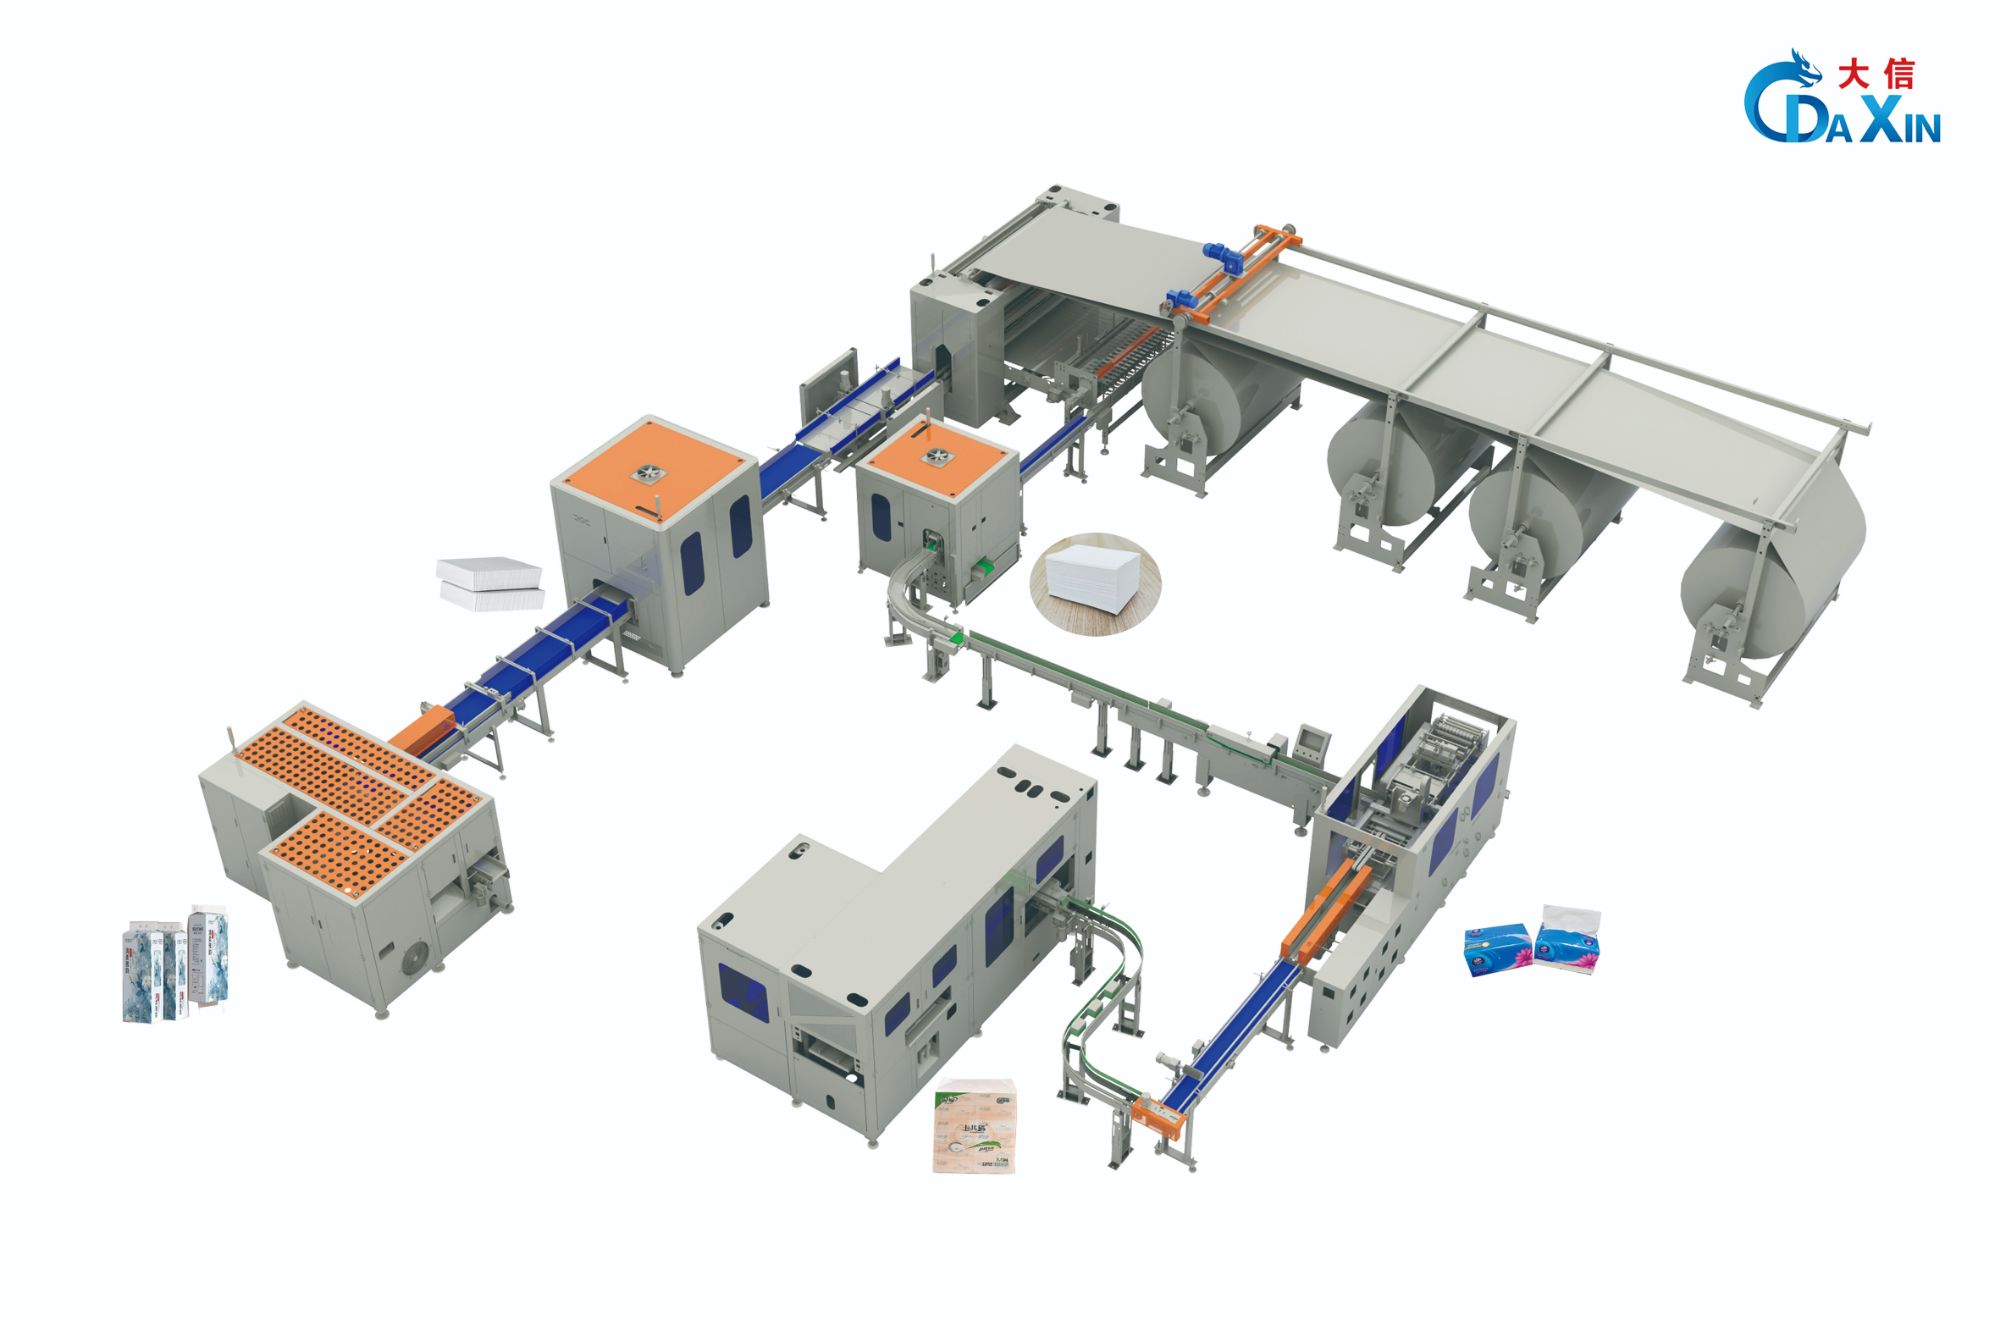
Most operators only notice web tension when something visibly goes wrong—wrinkles, baggy edges, or a sudden snap. But the real damage often happens in the background, long before a defect reaches the rewind. Subtle shifts in tension can alter coating weights, change register accuracy, or stretch substrates just enough that downstream converting steps produce scrap. It’s not a dramatic failure; it’s a slow bleed on yield that no one tracks until the monthly numbers look off.
A common misconception is that tighter always means better control. In reality, excessive tension can permanently deform films, crush lightweight papers, or cause telescoping in rolls that look perfect at first glance. On the flip side, too little tension lets the web wander, creating edge flutter that throws off sensors and guides. The machine keeps running, the operator adjusts something else, and productivity quietly erodes because the true root cause never gets addressed.
What makes this sabotage so insidious is that it hides in plain sight. Tension is not a single setting—it varies with roll diameter, speed changes, splice events, and even ambient humidity. Without continuous monitoring or a clear mapping of tension zones across the line, a web can drift out of spec for hours, producing output that passes basic inspection but fails in the customer’s process. By the time the problem becomes obvious, thousands of feet of material may already be compromised.
Embossing Rolls That Don't Wear Out Mid-Shift
Ever had an embossing roll give up halfway through a production run? The pattern starts to soften, edges lose their crispness, and suddenly you're scrapping batches or slowing the line. That mid-shift failure isn't just an inconvenience—it's a profitability killer. The good news is that modern embossing rolls can be engineered to shrug off the daily grind. We're talking about substrate-specific hardening, precision crown grinding, and surface treatments that keep those fine details sharp from first impression to last.
What separates a roll that lasts a full shift from one that fades early often comes down to microstructure. A uniform, deep-case hardening profile prevents localized wear on high-point contacts. Add in a low-friction coating—whether it's a engineered chromium or a ceramic-based layer—and you cut down the micro-abrasion that dulls patterns over hours of continuous contact. Pair that with internal cooling channels designed for your exact line speed, and the roll stays dimensionally stable, not just hard. That stability is what keeps register tight and rejection rates flat, even on long runs.
The payoff isn't just fewer roll changes. It's a quieter shift—fewer alarms, less manual inspection, more consistent output from the first pallet to the last. And when you're not swapping rolls mid-run, you're not losing the thermal equilibrium that fine embossing depends on. So the next time you spec a replacement, don't just ask for 'hardened steel.' Ask how that hardness is distributed, how the surface reacts under load, and what happens at hour six of an eight-hour run. That's where the real difference hides.
Dust Control Without Sacrificing Throughput
For years, the trade-off seemed unavoidable: either you contained the dust and watched your tonnage dip, or you kept the line moving and accepted the haze. Many operations simply learned to live with both problems, patching leaks and adjusting speeds in a never-ending cycle. That kind of compromise quietly eats into margins, because slowdowns aren't just inconvenient—they compound across every shift.
The shift happens when dust control is designed into the flow path rather than bolted on afterward. Sealed transfer chutes, properly sized pickup points, and airflow that moves with the material instead of against it can capture fines at the source without creating a bottleneck. In well-tuned systems, the material keeps its velocity, the belt stays loaded, and the dust never gets a chance to escape into the surrounding air.
What often gets overlooked is how much dust-related wear and tear was already costing in hidden downtime. Bearings, idlers, and sensors last longer when they aren't coated in abrasive fines. The goal isn't to add more extraction power—it's to use the right amount of suction at the right moment, so you're not pulling product off the belt or wasting energy. When the balance is right, throughput stays flat or even improves while the air clears up.
Knife Life as an Overlooked Efficiency Metric
In most kitchens, the condition of a knife rarely makes it onto the list of things that get measured. Yet the dullness of a blade quietly dictates how long every single cut takes. A chef working with an edge that has lost its bite will naturally compensate with more force, more sawing motions, and more repositioning of the food. Those extra seconds per slice pile up across a prep list until an entire hour has evaporated. Knife life, then, isn't just about maintenance schedules—it's a live metric of workflow friction that most teams never bother to track.
Consider the difference between a knife that holds its edge for two weeks versus one that needs honing every other day. The measurable gap isn't in sharpening time alone; it's in the stolen momentum of every task that follows. A cook who trusts the blade to fall through an onion without resistance can keep a rhythm that feels almost mechanical. That same cook, fighting a rolled edge, will break that rhythm dozens of times per shift. Over a month, the accumulated hesitation shows up not in a logbook but in later ticket times, rushed plating, and fatigue that no amount of caffeine can fix.
Measuring knife life forces a conversation about what actually slows a kitchen down. Instead of buying cheaper blades and replacing them constantly, a team that tracks edge retention starts to see the real cost of downtime. It forces choices about steel type, honing frequency, and even who gets assigned the heavy prep. None of this appears on a traditional efficiency report, but anyone who has worked a busy line knows the difference immediately. The knife is a small instrument with an outsized effect on speed—and ignoring its lifecycle is a quiet way to accept mediocrity.
Why Modular Design Beats One-Size-Fits-All
A one-size-fits-all product often looks efficient on paper because it streamlines manufacturing and reduces upfront choices. But that efficiency usually comes at the expense of the people actually using it. Modular design starts from the opposite end: instead of forcing everyone into the same mold, it breaks a system into swappable, self-contained pieces. That means a musician can add extra inputs to a synthesizer, a homeowner can replace a single drawer front instead of an entire kitchen cabinet, or a factory can upgrade one sensor array without shutting down the whole line. The result is less waste, both in materials and in frustration, because the product adapts to the task rather than the other way around.
There's also a quiet economic logic that gets missed in the initial sticker-price comparison. Modular systems tend to have a higher entry cost for the base unit, but they spread the real investment over time. When a part breaks or a need changes, you buy the module, not the machine. Over a decade, that can mean thousands of dollars saved and far fewer items sent to landfill. The one-size-fits-all approach locks you into a single lifecycle; modular design gives you a platform that evolves. That's why it appeals not just to hobbyists who enjoy tinkering, but to procurement managers and engineers who need equipment that won't become obsolete after one design cycle.
FAQ
A converting line unwinds large parent rolls and transforms the web into finished toilet paper, kitchen towels, napkins, or facial tissue through embossing, perforating, folding, cutting, and packaging. Efficiency often slips at reel changes, embosser synchronization, and folding accuracy. Addressing those transitions and alignment points usually yields stronger throughput than simply running the line faster.
Focus on automatic reel splicing, precise tension control, and servo-driven folding units. Replacing pneumatic or mechanical adjustments with closed-loop feedback prevents small deviations from turning into jams. Also upgrading perforation blades to longer-wear materials cuts unplanned stops more than many operators expect.
Every minute spent switching embossing patterns, fold types, or sheet counts is time the line is not producing saleable rolls. Tool-less change parts, recipe-based servo positioning, and color-coded guides can reduce a 40-minute changeover to under 10 minutes. On short runs, that shift often boosts weekly output by 15 to 20 percent without increasing line speed.
Vibration analysis on embosser bearings, routine inspection of folding fingers, and torque checks on cutting drums prevent small wear issues from becoming breakdowns. Plants that track roll quality metrics and change consumables on a condition basis rather than a fixed calendar usually hold higher uptime, because they catch dull blades and worn belts before defects appear.
Yes, if the line is designed with modular folding plates, adjustable embossing stations, and recipe-controlled servo axes. The key is not just flexibility but repeatability: positions must return to the same settings after every changeover. Without stored recipes and absolute encoders, operators tend to make manual tweaks that create variability and speed losses.
Common bottlenecks include the log saw, packaging infeed, and tail sealing. The converting section may be fast, but if finished rolls queue up before wrapping, the line still loses output. Solving this often means balancing downstream accumulation, adding buffer conveyors, and synchronizing wrapper speed with the converting line rather than treating them as separate islands.
Modern control systems collect real-time data on stops, speed, waste, and quality, then display the biggest losses on a single screen. This makes it easier for crews to prioritize the right issues. Automatic slowdown before a predicted jam, synchronized line speed, and remote diagnostics also reduce the time spent troubleshooting, so experienced operators focus on improvements instead of firefighting.
For many mills, yes. Replacing the control platform, upgrading tension control, and adding automatic splicing can extend a machine's useful life at a fraction of new line cost. The return is faster when the retrofit targets the top three causes of downtime rather than trying to modernize everything at once.
Conclusion
High-speed tissue converting lines rarely bog down because the drives or motors hit a ceiling. The real reason is the sheet itself: at elevated speeds, small imbalances in web tension grow into flutter, edge wrinkles, and snap-offs that force operators to dial back. Tension is not a set-and-forget parameter. Slight drift across unwind splices or roll build-up quietly erodes throughput, and the typical response—cranking up tension—only masks the problem until a break occurs. A smarter line treats tension as a dynamic loop, using load-cell feedback and dancer positioning to absorb disturbances before they reach the converting stations.
Embossing rolls that lose pattern sharpness halfway through a shift trigger quality checks and slowdowns, so hardened surfaces and precision alignment matter more than initial pattern depth. Dust control, often treated as housekeeping, becomes a throughput issue when vacuum hoods or brushes restrict airflow or need constant cleaning; extracting dust right at the slitting point keeps it from accumulating without choking the line. Knife life is an equally telling metric—frequent blade changes add up to hidden hours that rarely show up in standard efficiency reports. Finally, modular design lets a plant swap in a new unwind, embosser, or folder without re-engineering the entire layout, which beats forcing one rigid configuration to handle every product grade.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/