Stainless Steel Self Tapping Screws Factory: A Guide to Manufacturing Excellence
2026-11-16
Most guides to stainless steel self-tapping screws stop at specs and thread counts. This one goes inside the factory floor—where raw wire becomes fasteners that hold everything from EV battery trays to coastal decking. At Wanluo, manufacturing excellence isn't a slogan; it's measured in burr-free points, consistent case hardness, and salt-spray hours that exceed the datasheet. If you've ever wondered why two screws with the same DIN number perform differently in the field, the answer usually starts here. Read on for a behind-the-scenes look at the processes, tolerances, and quality checks that separate a reliable supplier from a costly gamble.
Raw Material Traceability That Prevents Mixed-Grade Failures
Every batch of incoming raw material carries its own fingerprint—supplier lot, grade designation, and even the specific production line it came from. If that fingerprint gets smudged or lost between the warehouse and the blending station, you're setting yourself up for a costly mix-up. The real trick isn't just recording the data; it's making it impossible to skip a step without the system raising a flag. For example, forcing a barcode scan at each transfer point and automatically cross-checking it against the job's material requirement can stop a lower-grade resin from ever reaching a high-spec compound line.
But traceability isn't only about catching mistakes after they happen. A well-designed system builds a chain of custody that's visible to the operators in real time. When someone on the floor sees a red warning that the scanned lot doesn't match the approved grade for that work order, they don't need to guess or ask a supervisor. The decision to halt or investigate is immediate. That kind of instant feedback reduces the temptation to 'just use it anyway' when the correct material is a few aisles away.
Finally, the payoff comes during audits and customer complaints. Instead of digging through paper logs and hoping the shift notes were filled out, you can pull up a complete material genealogy for any finished batch in seconds. Show exactly which lot of each raw material went in, when it was checked, and by whom. That level of transparency doesn't just satisfy a certificate—it gives your team the confidence to say with certainty that no mixed-grade failure slipped through the cracks.
Cold Forming Angles That Reduce Thread Chipping
Thread chipping in cold-formed parts rarely starts at the root; it begins where the die angle forces material to fold over itself. By adjusting the lead-in angle to a shallower ramp, the blank enters the forming zone with less abrupt displacement, which spreads the deformation across more of the flank. This reduces the local tensile strain at the crest and keeps the grain flow continuous instead of tearing it apart.
The flank angle plays a similar role but works on a finer scale. A slightly reduced flank angle—often just a degree or two below the final thread form—gives the material room to flow upward without colliding with the die face. That collision is what initiates micro-cracks at the thread tip. Equally important is the relief angle behind the forming edge; too sharp a relief drags material backward, while a properly radiused relief lets it release cleanly and prevents micro-chipping along the top edge.
In practice, these angles are not set once and forgotten. Higher-strength alloys demand a longer, more gradual lead-in because their reduced ductility triggers chipping at smaller strain gradients. Tool wear changes the effective angles as well, so monitoring the first signs of crest flaking often points back to a worn lead-in or a relief that has lost its radius. Adjusting those angles early preserves thread integrity far better than increasing forming pressure.
Heat Treatment Cycles That Avoid Carbide Precipitation
Carbide precipitation in stainless steels and nickel alloys is not a simple function of temperature alone; it also depends heavily on how long the material lingers in the vulnerable range. A practical heat treatment cycle therefore places the emphasis on speed through the 450–850°C window. Instead of slow furnace cooling after solution annealing, the workpiece is rapidly quenched—often in water or forced air—so that carbon remains trapped in solid solution and never gets the chance to diffuse to grain boundaries. The result is a cleaner microstructure without the characteristic chromium-depleted zones that invite intergranular attack.
For alloys that cannot be quenched aggressively due to distortion concerns, staged cooling offers a middle path. The part is held briefly at a temperature above the sensitization range to equalize, then cooled rapidly through the critical band before a slower, controlled cool at lower temperatures. Some fabricators also use stabilization heat treatments with titanium or niobium additions, but even these require careful cycle design: the stabilization anneal itself must avoid lingering in the precipitation nose of the time-temperature curve. In every case, the goal is the same—engineer the thermal path so that the material spends as little time as possible where carbides want to form.
Drive Recess Geometry Checks Under Production Speed
Verifying recess geometry on drive components used to mean pulling parts off the line for a bench inspection, a process that rarely kept pace with modern production cadence. The real challenge isn't just measuring the depth or angle of a recess—it's doing so while the part moves at full throughput, without disrupting the flow or introducing operator-dependent variability.
One practical approach uses a compact laser profilometer mounted directly above the conveyor. As each drive passes beneath, the sensor captures hundreds of cross-sectional profiles in milliseconds, reconstructing the recess contour against a stored CAD reference. Deviations in wall angle, fillet radius, or floor flatness trigger an immediate pass-fail output, with the raw point cloud archived for traceability.
The payoff is not just speed but consistency. By embedding geometry checks into the production line rather than alongside it, manufacturers catch dimensional drift on the first part instead of the fiftieth, reducing scrap and avoiding the hidden cost of late-stage rework. Recess features that once demanded a dedicated inspection station now clear verification in the same cycle time as a standard part transfer.
Passivation Bath Monitoring for Consistent Oxide Layers
Passivation baths quietly shift composition with every rack that passes through, and if nobody is tracking that drift, oxide thickness starts to wander. A monitoring routine that logs pH, temperature, and dissolved metal content at fixed intervals catches small deviations before they translate into uneven color or weak spots. The goal is not to chase perfection, but to keep the bath inside a window where the oxide forms predictably.
Regular titration of the free acid and oxidizer, paired with a conductivity check and visual inspection of bath clarity, gives a surprisingly complete picture without expensive equipment. For lines running high volumes, adding an automatic dosing controller tied to those readings removes much of the operator-to-operator variation. Monitoring also flags contamination early—chlorides, drag-in from previous tanks, or organic buildup—each of which can sabotage an otherwise healthy passivation process.
The real payoff shows up in downstream performance. When the bath stays inside its control limits, oxide layers come out uniform in thickness and color, and corrosion resistance becomes repeatable across batches. That consistency reduces rework downstream and makes failure analysis much simpler because the surface preparation step is no longer the first suspect.
Torque-to-Failure Sampling That Predicts Field Performance
Bolted joints rarely fail exactly where the design spreadsheet says they will. Torque-to-failure sampling pulls a small number of production fasteners and drives them past their intended seating torque until the threads or head strip. The resulting distribution captures real variation in friction, plating thickness, and thread fit, not the idealized values assumed during engineering.
On the line, operators or automated stations run this test at set intervals—every shift, every batch, or after a tool change. The torque and angle at failure are logged against the joint’s specification limits. Over time, these data points reveal drift before it becomes a field issue, like a change in coating vendor reducing friction and shifting the failure window lower than expected.
What makes this valuable is the direct link to warranty and service life. A joint that barely passes its target torque in the plant may loosen after thermal cycling or vibration. By tracking the margin between assembly torque and failure torque, engineers can predict which batches are likely to underperform in the field and adjust calibration or supplier processes accordingly.
FAQ
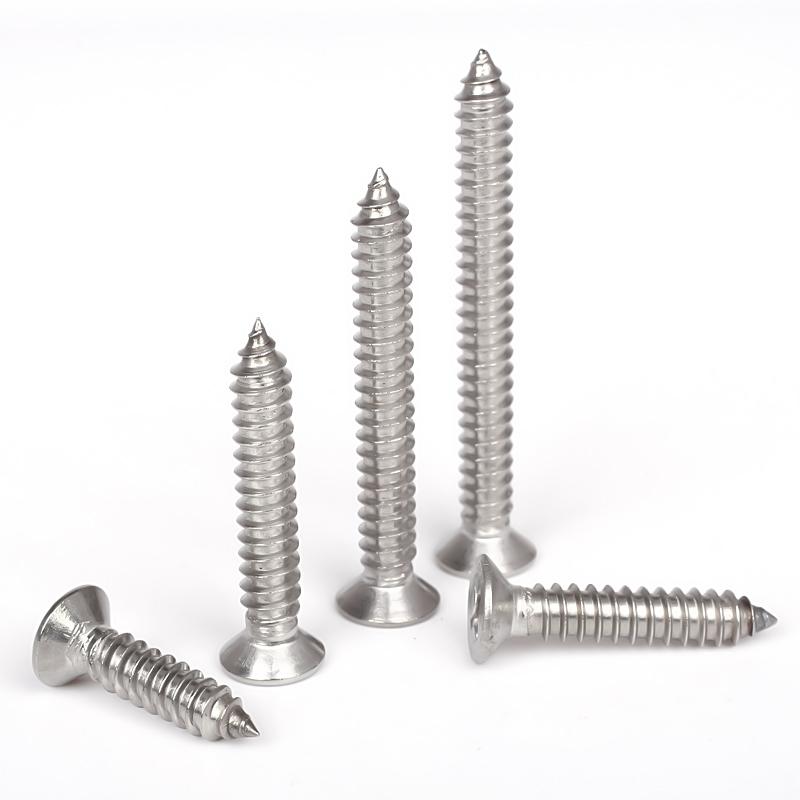
The core difference lies in their ability to cut or form their own mating threads as they are driven into materials like metal, plastic, or wood. Regular screws typically require a pre-tapped hole or a nut. Stainless steel self tapping screws have a specially designed point and thread geometry that displaces material rather than removing it, which creates a tight fit and reduces the need for additional fastening components.
Consistency in thread quality starts with precision tooling and rigorous process control. The factory typically uses cold heading machines with tightly maintained dies, and then rolls the threads rather than cutting them. Thread rolling compresses the steel grain structure, making the threads stronger and more uniform. In-process inspections using optical comparators or laser micrometers check pitch diameter, flank angle, and lead error at regular intervals. Any drift in tooling or machine settings triggers an immediate stop and adjustment.
The two most common grades are 304 and 316. Grade 304 offers good corrosion resistance for general indoor and mildly outdoor environments, and it is easier to cold form, which keeps production costs reasonable. Grade 316 contains molybdenum, which significantly improves resistance to chlorides and acidic conditions, so it is chosen for marine, chemical, or food processing applications. Some factories also offer 410 stainless steel when higher hardness and wear resistance are needed, though its corrosion resistance is lower.
The process generally begins with wire drawing to reduce stainless steel coil to the correct diameter and improve surface finish. Next, cold heading forms the screw head and blank shank in a multi-station machine. The point is then shaped, often by a secondary pointing operation, to create the cutting or piercing geometry. Thread rolling follows, which forms the threads under high pressure. After that, screws may undergo heat treatment if hardening is required, though many austenitic stainless grades are work-hardened instead. Finally, cleaning, passivation, and optional coating or lubrication are applied before packaging.
Performance testing usually covers three main areas: drive torque, thread forming ability, and pull-out strength. Factories use torque testers to measure the force needed to seat the screw without stripping. They also perform repeated insertion and removal cycles in representative materials to check for thread damage or galling. Salt spray tests evaluate corrosion resistance over hundreds of hours. For critical applications, vibration tests and tensile tests on assembled joints are conducted to confirm the screw holds under dynamic loads.
One major challenge is preventing the screw point from becoming brittle during cold forming, especially in harder stainless grades. Factories address this by controlling the degree of deformation and using intermediate annealing when necessary. Another challenge is galling, where the screw thread fuses to the mating material due to friction and pressure. This is managed by applying specialized dry film lubricants or wax coatings. Dimensional drift in thread rolling dies is also common, so factories monitor die wear closely and replace tooling before it affects thread geometry.
Buyers should look beyond polished marketing materials and ask for concrete evidence. A factory with a strong commitment will readily share its quality control plan, including sampling rates, inspection equipment calibration records, and traceability procedures from raw material heat numbers to finished lot codes. Visiting the production floor often reveals a lot: clean work areas, organized tool storage, and operators who can explain their inspection points. The factory should also be willing to discuss failure modes they have encountered and how they corrected them, which shows honest problem-solving rather than hiding behind claims of zero defects.
Heat treatment is not applied universally because austenitic stainless steels like 304 and 316 cannot be hardened by quenching and tempering the way carbon steels can. For these grades, work hardening from cold forming already provides sufficient strength for most self tapping applications. However, martensitic stainless grades such as 410 do require heat treatment to achieve the necessary hardness for the cutting point and threads. The process involves austenitizing, quenching, and tempering, followed by passivation to restore corrosion resistance. Factories must carefully control furnace temperatures and atmosphere to prevent carbide precipitation or scaling.
Conclusion
Achieving true manufacturing excellence in stainless steel self-tapping screws starts well before the first thread is formed. Traceability systems that track each heat of raw material from mill to production line eliminate the risk of a lower-grade alloy slipping into a high-performance batch, which would otherwise cause premature corrosion or field failure. Once the correct material is confirmed, cold forming tooling is carefully angled to prevent micro-chipping along the thread flanks, preserving the sharp, clean cutting edges that self-tapping screws depend on. Equally critical is the heat treatment cycle, where temperature and time are tightly controlled to avoid chromium carbide precipitation at grain boundaries. This step alone can mean the difference between a screw that resists rust for decades and one that begins to pit after a single season.
Final inspection goes beyond visual checks. Drive recess geometry is verified under actual production speed using non-contact measurement, so a worn punch or misaligned tool cannot ship thousands of sockets that would cam out in the field. Passivation baths are monitored continuously, not just sampled once per shift, to keep the oxide layer uniform and free of iron contamination that would compromise the passive film. The most telling quality gate, though, is torque-to-failure sampling on finished screws. By driving them into calibrated test plates and measuring the exact failure point, the factory can predict not just whether a screw will hold, but how much margin it carries under real installation stresses. Together these checks turn a commodity fastener into a repeatable, field-proven component.
Contact Us
Contact Person: Shane
Email: [email protected]
Tel/WhatsApp: 8613357785029
Website: https://www.wanluohardware.com