OA Network Floor Factory: Durable Raised Floor Systems for Modern Workspaces
2026-09-13
Every modern workspace hides a secret below its surface—a network of cables, airflow, and structural support that keeps everything running. But what happens when that hidden layer can't keep up? That's where a truly durable raised floor system makes all the difference. As you plan your next office build-out or renovation, the choice of OA network floor manufacturer matters more than you think. Lipin Floor has spent years perfecting raised access flooring that doesn't just meet specs—it anticipates the messy reality of daily use. Let's dig into what separates a floor you forget about from one you constantly worry about.
Built to Outlast Constant Office Traffic
In high-traffic office environments, furniture endures constant use from early morning meetings to late-night deadlines. Chairs roll across hard floors, desk edges get bumped by bags and elbows, and drawer runners are opened dozens of times a day. A product built to outlast this traffic isn't just about thick materials—it's about choosing the right joints, reinforcements, and surface treatments that quietly absorb daily abuse without showing wear. The goal is furniture that still looks and functions like new after years of nonstop activity, not something that needs replacement every few seasons.
The secret lies in understanding exactly where office furniture fails first. Armrests crack from repeated leaning, laminate edges peel after countless collisions, and casters clog with dust and fibers from carpet. Designing for longevity means reinforcing those weak points with metal brackets where plastic would snap, using edge banding that resists impact rather than just covering raw board, and selecting casters with sealed bearings that keep rolling smoothly through debris. It also means testing prototypes not in a lab with gentle simulation, but in real offices with real people who don't treat furniture with kid gloves.
Beyond materials, modular construction plays a huge role. When a single component wears out—a worn arm pad, a scratched worksurface, a sticky drawer slide—it should be replaceable in minutes without special tools or entire unit teardown. This approach reduces downtime and avoids the cycle of discarding whole pieces over minor damage. In the end, furniture that withstands constant office traffic isn't a luxury; it's a practical investment that keeps workspaces looking professional and functioning smoothly, year after year.
Where Cable Management Meets Panel Strength
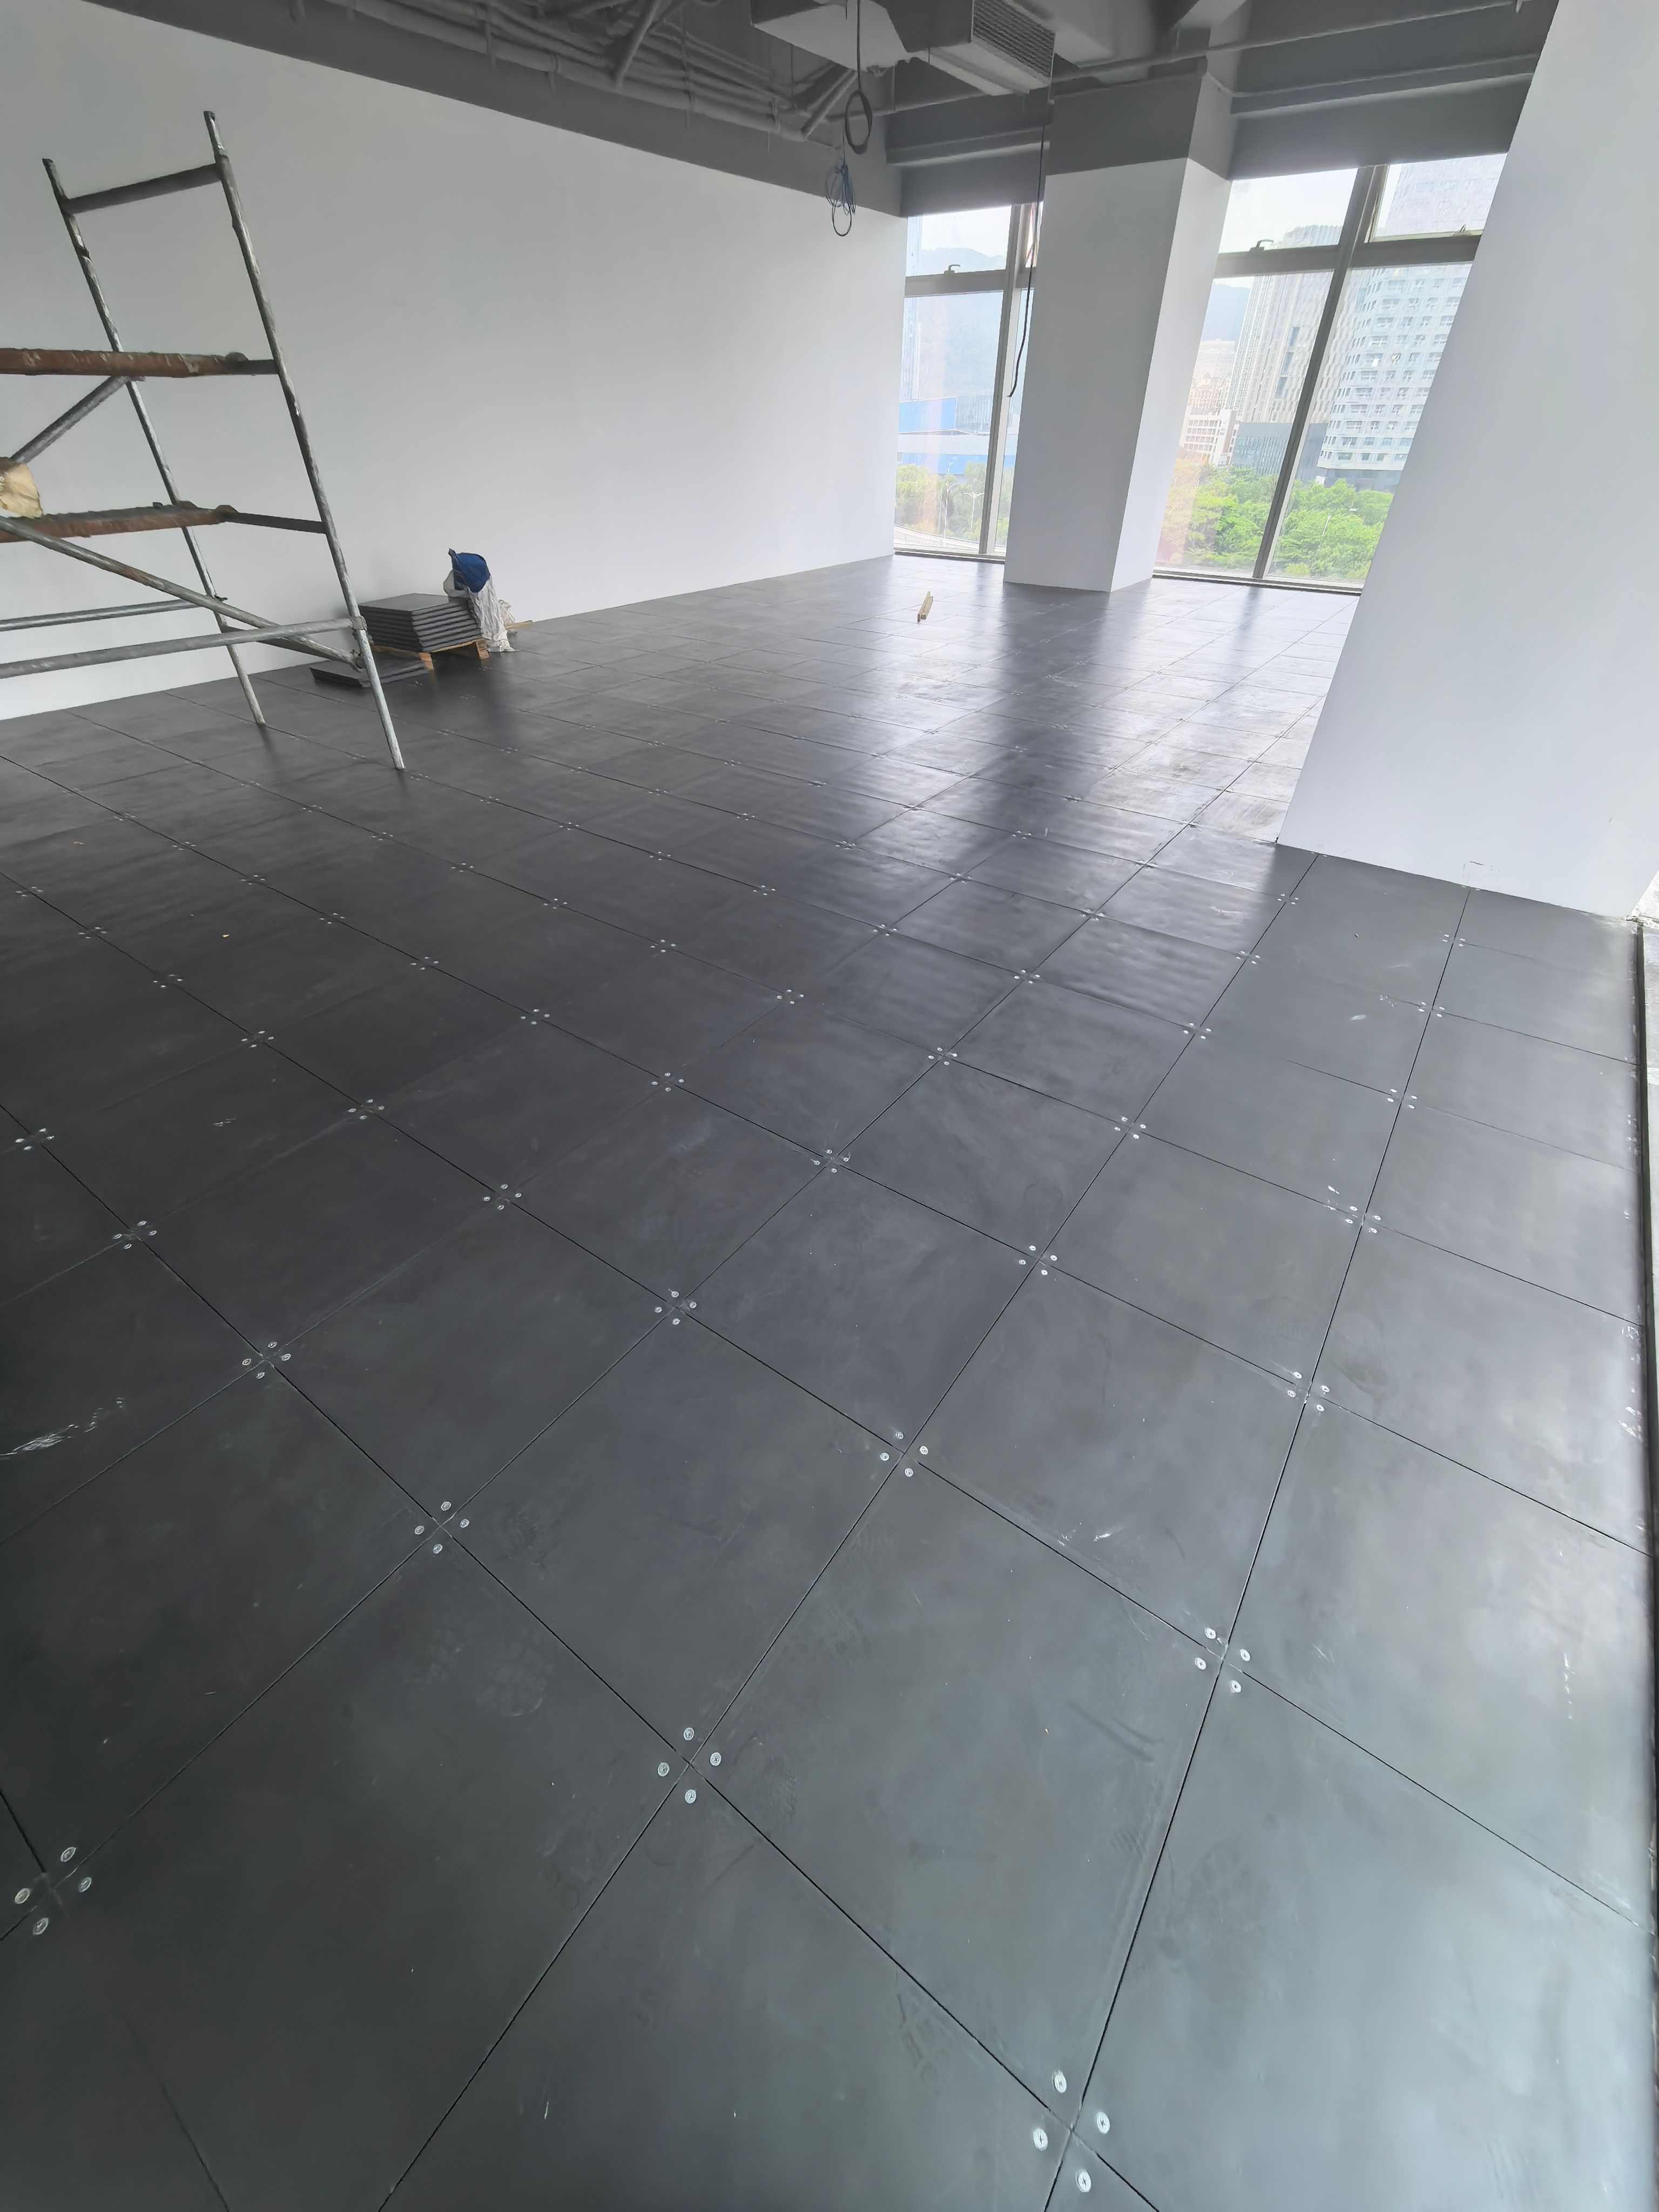
Most panels treat cable routing as an afterthought—cutouts stamped into steel with sharp edges that chew insulation over time. Here, the structure itself is the pathway. Reinforced channels are pressed into the panel face, creating a rigid backbone that guides power and data lines without adding bulk. The result is a surface that stays flat under load yet directs every cord exactly where it needs to go.
The real difference shows up when you mount heavy equipment. Instead of sagging or flexing around open slots, the panel's formed ribs lock into the frame, distributing weight while leaving generous clearance for bundles. Cable ties anchor into recessed points, so there is no zip-tie chaos spilling over the edges. You can trace any run by eye and still have room to spare for future additions.
What makes this work is a deliberate overlap: every bend that stiffens the metal also softens the path for cables. Edges are rolled, not raw. Corners are radiused to prevent pinch points. The panel ends up doing double duty—half load-bearing skin, half quiet organizer—without forcing you to choose between a clean install and a strong one.
Inside the Factory: How Each Panel Gets Tested
Walk onto the factory floor and the first thing you notice is the hum of the laminator and the faint smell of heated EVA. Every panel moves along the line on a steel cart, but before it reaches the test bay, an operator checks the barcode against the batch sheet. This isn't busywork; a single misplaced serial number can send a good panel to the reject pile.
The actual testing starts with a dark-room flash test. A xenon lamp fires for about 10 milliseconds, simulating full sunlight, and the resulting I-V curve gets compared to a golden reference module. If the curve has even a small kink, the panel is pulled aside for electroluminescence imaging. That's where you see micro-cracks that would otherwise stay hidden. Technicians here joke that EL photos are 'panel X-rays' because they reveal breaks invisible to the naked eye.
After electrical checks, panels go through a climate chamber that cycles from -40°C to 85°C while humidity is pushed to 85%. The chamber's door seals make a soft hiss when they open, and the operator logs the thermal cycle count on a clipboard, not just a computer, as a backup. Only panels that pass all three stages get a final visual inspection under angled LED light, then a stamp with the date and tester's initials.
Fit for Renovations and New Builds Alike
Most building products quietly assume you are starting from a clean slate. That assumption collapses the moment you open up a 1970s bathroom or try to meet a tight framing schedule on a new build. This system was developed around a different question: how do you make one approach work when the subfloor is wavy, the existing tile is staying put, and the crew still has three other trades waiting behind them? The answer came from designing tolerances and connection details that absorb the messiness of renovations without slowing down the clean, predictable rhythm of new construction.
On renovation sites, that means you can often go right over sound existing flooring instead of tearing it out, which keeps dust, skip hire, and labour costs in check. On new builds, the same components slot into standard framing and drywall sequences without forcing a change order just to accommodate a niche installation method. The result is a single specification that architects can drop into a Victorian terrace retrofit or a three-storey infill project and still get the same finished look and performance, without the usual caveats.
Surface Options That Handle Real Daily Wear
Daily life isn't kind to surfaces. Coffee rings, key scratches, muddy paw prints, and the occasional dropped pan all leave their mark. The right surface choice turns that chaos into background noise, not a constant maintenance project.
Quartz and porcelain slabs have earned their place in busy kitchens and baths for good reason. They shrug off stains, resist chips better than natural stone, and never ask for sealing. For those who prefer the warmth of wood, thermally modified ash or oak offers a tougher, more stable alternative that handles spills and humidity without warping.
In high-traffic zones, matte laminate and compact laminate panels deliver a practical edge. They absorb impact quietly, hide fingerprints well, and clean up with a simple wipe. Choose a textured finish over high gloss, and the inevitable smudges and fine scratches become nearly invisible, extending the life of the look without extra effort.
Why Direct Factory Support Changes the Timeline
Direct factory support strips out the relay race that usually slows down custom projects. When a distributor sits between you and the production floor, every question about materials or scheduling has to pass through an extra pair of hands. Removing that layer means the factory starts planning your order the same week it's placed, not after a backlog of forwarded emails.
There's also a difference in how quickly problems get solved. A factory team talking straight to the buyer can flag a supply hiccup in the morning, offer two workable alternatives by lunch, and keep the production slot intact. That kind of real-time adjustment is what cuts a typical eight-week lead time down to three or four, without the usual approval limbo.
FAQ
The panels combine a steel shell with a dense calcium sulfate core, so they resist dents and edge damage even when office chairs roll over them all day. The factory also applies a scratch-resistant coating to keep the surface looking clean through years of rearrangement.
Yes. Each panel lifts out individually, which gives your IT team quick access to power and data lines without disrupting the whole floor. Ventilated panels can be swapped in wherever cooling is needed, so the layout stays flexible as teams grow or move.
The pedestals adjust to compensate for uneven subfloors, and the panels click into place without wet trades. Most standard offices can be covered in a few days, and the factory provides detailed layout drawings to minimize cutting on site.
You can choose from high-pressure laminate, vinyl, rubber, or carpet tile finishes. Many clients order anti-static surfaces for electronics-heavy areas, and custom colors or wood-look textures are available for reception zones.
Standard panels handle concentrated loads around 1,000 pounds, while heavy-duty versions go up to 3,000 pounds or more. The exact rating depends on the core material and panel size, and the factory can help you pick a grade matched to rolling file cabinets or server racks.
Very little. Sweep or vacuum the surface regularly, and occasionally lift a few panels to check that pedestals remain level. If a panel gets damaged, you just replace that single piece instead of redoing the entire floor.
Working directly with the factory means you skip middleman markups and get straight answers on load ratings, lead times, and custom cuts. The production team can also adjust panel dimensions mid-project without long delays.
Conclusion
Walk through any busy office and the floor takes more punishment than almost any other surface. OA Network Floor Factory builds raised access floors with that reality in mind. Every panel is assembled and then pushed through a series of load, edge, and impact checks before it leaves the production line—not just sampled, but tested one by one. The result is a system that keeps its flatness under constant chair traffic, rolling carts, and the occasional dropped tool. Beneath the surface, cable trays and cutouts are integrated into the panel structure rather than added as an afterthought. That means running power, voice, and data lines underneath doesn't weaken the deck or create uneven seams. It also keeps the workspace adaptable without tearing up concrete or chasing walls.
Renovation projects and ground-up builds both benefit from the same modular approach. Panels can be leveled over existing slabs, adjusted for new service requirements, or matched to a range of surface finishes that are chosen for real daily wear—textured laminates that resist scuffs, static-dissipative options, and materials that don't show every footprint. Because the factory sells directly, there is no wait for a distributor to check stock or route a question. A change in panel count, a custom cutout for a column, or a revised delivery window can be handled by the same team that actually schedules production. That direct line shortens lead times and prevents the usual back-and-forth that drags out fit-out schedules. For facility managers and contractors, it means the floor arrives when expected and stands up long after installation.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/