Isopropylated Triphenyl Phosphate Company: Key Factors to Consider for Your Supply Chain
2026-10-31
Isopropylated triphenyl phosphate may fly under the radar in your BOM, but the wrong supplier choice can stall production or trigger compliance headaches. That's why leading formulators now treat IPTPP sourcing as a strategic lever, not a commodity purchase. Fortune has engineered its supply chain around the factors that keep your lines running and your specs intact. Before you sign the next PO, consider these often-overlooked criteria.
Supplier Transparency Beyond the Spec Sheet
A spec sheet tells you what a supplier claims to deliver, but it rarely shows how they actually work. Real transparency means walking the floor without a script—watching how materials are handled, how operators troubleshoot, and whether the safety posters match the behavior. One visit where you ask a line worker about their last audit result can reveal more than a stack of compliance documents.
Beyond the paperwork, transparency grows from shared problem-solving. When a supplier admits a delay in raw material shipments before it becomes a crisis, or invites you to a pre-production trial run, that's where trust is built. It's less about checking boxes and more about having the kind of relationship where bad news travels fast—because the supplier knows you'll help fix it, not just penalize it.
Why Batch Consistency Outweighs a Low Quote
A supplier who quotes rock-bottom prices but delivers a different product every run will quietly drain your budget through rework, returns, and customer complaints. One batch may cut, bend, or finish perfectly; the next drifts outside tolerance and forces you to babysit the line. The cheap quote stops looking cheap when you are paying twice for the same order.
Consistency, by contrast, compounds in value. When the third shipment matches the first exactly, your assembly crew moves faster, your quality checks shrink to spot audits, and your own customers learn they can trust what they receive. That trust is worth far more than the few cents per unit you might save by chasing the lowest number on a spreadsheet.
The smart calculation includes the cost of variability. Ask any production manager who has had to quarantine a container or apologize for a delayed launch: a stable process, documented raw material sources, and locked-in tooling beat a discount that disappears under the weight of one bad batch.
Regulatory Pressure Points Impacting Phosphate Esters
The most immediate pressure comes from chemical safety assessments in the EU and North America, where several chlorinated phosphate esters—most notably TCEP and TDCPP—have been designated as Substances of Very High Concern under REACH or listed under California Proposition 65. These listings trigger mandatory labelling, phase-outs in consumer goods, and disclosures throughout the supply chain. Because these compounds were widely used as flame retardants in flexible polyurethane foam and electronics housings, the restrictions force formulators to either reformulate or lose access to key markets.
A second pressure point is occupational and environmental exposure limits. Volatile phosphate esters such as tributyl phosphate have drawn scrutiny for neurotoxic effects, prompting lower permissible exposure levels in industrial workplaces. Meanwhile, regulatory agencies in Europe and parts of Asia are tightening discharge limits for phosphate esters into surface water, driven by concerns over eutrophication and aquatic toxicity. These rules make existing process designs and fluid formulations non-compliant without significant investment in containment or substitution.
The cumulative effect is a shift toward non-halogenated and polymeric phosphate esters, which generally offer a more favourable toxicological profile but often fall short on flame-retardant efficiency or low-temperature flexibility. Manufacturers facing these regulatory pressure points are therefore compelled to balance performance, cost, and evolving compliance requirements—a dynamic that has already reshaped supply chains for flame retardants, hydraulic fluids, and plasticizers.
Logistics Blind Spots in Specialty Chemical Sourcing
Many procurement teams treat freight as an afterthought once the chemical grade and price are locked in. That habit creates blind spots almost immediately. Specialty chemicals often move under strict temperature, segregation, or packaging rules, and a carrier that looked cheap on paper may not have the right equipment or permits. A shipment of moisture-sensitive organometallics can arrive ruined if the trailer lacks a desiccant system, and no amount of supplier documentation fixes a rejected batch. The real cost shows up later as reorders, line stoppages, or emergency air freight that erases the initial savings.
Documentation is another area where blind spots accumulate. Specialty chemical sourcing involves more than a commercial invoice and a packing list. Depending on the route and mode, you may need Dangerous Goods declarations, TSCA or REACH-related statements, heat-treated pallet certificates, or specific labels for intermediate bulk containers. A missing or outdated document can hold a container at port for days, and detention fees start piling up. Even when the supplier has the paperwork, discrepancies between the supplier's description and the carrier's system often trigger manual inspections. Those delays rarely appear in the quoted lead time, yet they regularly consume more time than the actual transit.
Finally, the last-mile problem is amplified in specialty chemicals. Many production sites sit outside major logistics corridors, and regional LTL carriers may refuse hazardous or high-value chemical shipments altogether. If a lab needs fifty kilos of a custom catalyst in a rural industrial park, the options shrink fast. Procurement teams that only track ocean or main-carriage milestones miss the point where shipments stall on a cross-dock for a week. Building a small network of specialized forwarders or regional couriers who understand chemical handling is often the difference between a pilot project staying on schedule and a production trial waiting on a missing intermediate.
Total Cost Signals Hidden in Market Volatility
Most traders see a volatility spike and brace for wider spreads, but that reaction only scratches the surface. The real story sits inside the volatility surface itself—its skew, its term structure, how fast it shifts after large prints. Those shape changes leak information about the true cost of executing size, not just the quoted bid-ask. If you watch the front-month at-the-money straddle versus the back-month skew, you can spot when liquidity providers start charging a premium for inventory risk long before the tape shows it.
Think of market volatility as a slow-motion echo of order flow toxicity. When a large buyer works an order over several days, each slice leaves a footprint in the realized variance and in how option market makers adjust their wings. The cumulative effect shows up as a drift in implied correlation or a stubborn bid for out-of-the-money puts that has nothing to do with macro headlines. That drift is a direct read on the total cost of moving the underlying—impact, timing risk, and adverse selection bundled together—yet it rarely gets isolated from generic “uncertainty.”
Asset managers who ignore these embedded cost signals end up trading against their own footprint. A better approach treats volatility data as a running ledger of what the market charges for immediacy at different horizons. For instance, comparing the volatility risk premium across maturities against realized execution shortfall can reveal whether the crowd is underestimating the price of getting out of a large position quickly. That gap is where hidden total cost lives, and it shows up in the numbers before it ever shows up in a transaction cost analysis report.
Sourcing Strategies That Hold Up Under Disruption
When supply chains snap and lead times stretch beyond recognition, sourcing teams often learn a hard truth: the strategies that worked in calm markets are the first to collapse. The ones that endure share a common thread—they treat flexibility as a core requirement, not an afterthought. This means building a supplier base that isn't just cost-optimized, but deliberately redundant across geographies and tiers. A single-source component might save a few cents per unit, but that savings evaporates the moment a regional lockdown halts production for six weeks.
Another durable approach is shifting from transactional relationships to what some call 'co-development partnerships.' Instead of merely issuing purchase orders, leading companies share demand forecasts, engineering changes, and even risk registers with key suppliers. In return, those suppliers hold buffer stock, reserve capacity, or adjust production schedules on short notice. It's a mutual investment that pays off when disruptions hit, because both parties already have a playbook for rapid reconfiguration.
Finally, robust sourcing under disruption requires continuous scenario testing. Rather than auditing suppliers once a year against a static checklist, resilient organizations run quarterly 'stress drills' that simulate port closures, raw material shortages, or sudden demand spikes. The goal isn't to predict every crisis, but to build muscle memory for quick decisions—pre-approved alternate suppliers, standing logistics contracts, and clear escalation paths. That preparedness turns what could be a sourcing panic into a manageable operational pivot.
FAQ
Look beyond price per kilogram. A dependable partner should share batch-level purity data, have redundant production lines or multiple sourcing sites, and demonstrate a track record of on-time delivery even during raw material shortages. Ask for references from customers in your specific resin or foam system, not just general testimonials.
Different markets have different reporting requirements, especially in the EU and North America. Your supplier should provide full regulatory documentation—like REACH, TSCA, or local equivalents—without you having to chase them. If they cannot quickly clarify the substance's status for your application, that's a red flag.
Check isomer distribution, acid value, moisture content, and color. Isopropylated triphenyl phosphate can vary in performance depending on the alkylation pattern. A good supplier will provide a certificate of analysis that matches your processing window, not just generic industry specs.
In-house producers often give you more control over custom blends and faster troubleshooting. Distributors can be useful for smaller volumes or regional logistics, but you may lose visibility into the original manufacturing process. If you need consistent viscosity or flame-retardant loading, direct relationships usually work better.
Request third-party certifications or audit reports covering waste handling, emission controls, and raw material sourcing. Ask about their phosphorus recovery or recycling programs. A credible company will be willing to walk you through their production process, not just hand you a brochure.
Many buyers focus on price and forget about logistics fragility. This chemical can be sensitive to temperature extremes and long storage times. Verify that the supplier uses appropriate packaging, offers stability data, and has contingency plans for port strikes or shipping delays. Also check if they hold safety stock near your region.
Yes, reformulation and testing often eat up any upfront savings. If the new material has slightly different viscosity or phosphorus content, your processing parameters may need adjusting. Include trial costs, production downtime, and possible scrap rates in your comparison, not just invoice price.
Conclusion
Choosing an isopropylated triphenyl phosphate supplier is not just about comparing certificates. Real transparency means understanding how a producer manages raw material sourcing, controls isomer distribution, and handles trace impurities that never show on a standard COA. A plant audit or a shared process narrative often matters more than a polished data package. Batch consistency deserves more weight than an aggressive price. If phosphorus content, viscosity, or acidity drifts between lots, downstream compounding can suffer from erratic viscosity or plate-out, forcing rework that erases any upfront savings. Regulatory pressure on phosphate esters continues to shift, especially around impurity limits and exposure scenarios. A supplier who tracks evolving EPA and EU frameworks and flags possible reformulation risks before they reach your inbox is worth far more than one who simply passes along a compliance statement.
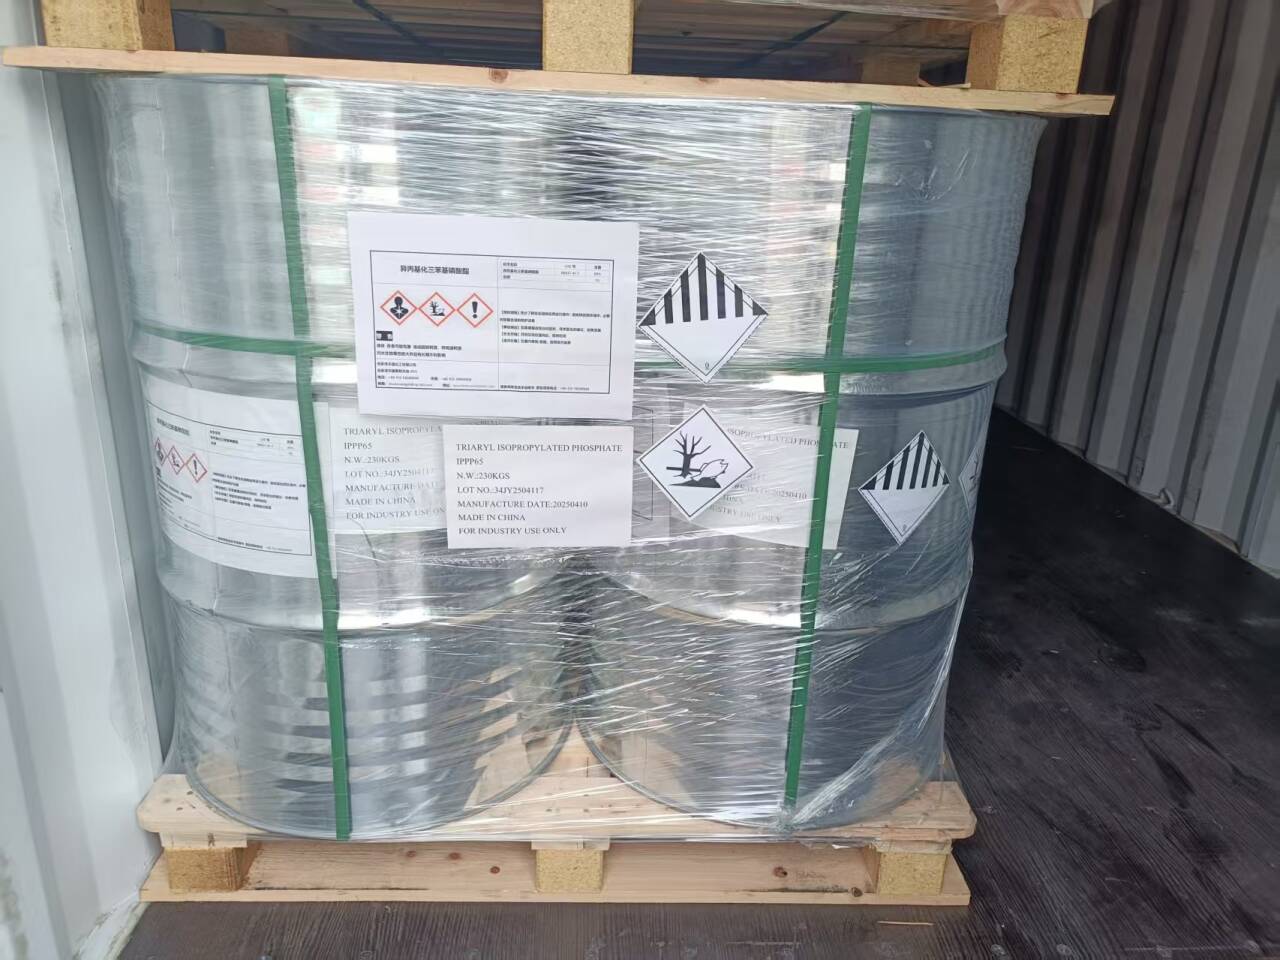
Logistics can quietly unravel a specialty chemical supply chain. Isopropylated triphenyl phosphate is often shipped in lined drums or isotanks, and moisture contamination or long dwell times at ports can degrade acid value or cause settling. Ask about regional warehousing, emergency transloading, and batch traceability during transit. On pricing, do not anchor on a single low quote; phenol and propylene markets move, and a supplier's ability to offer indexed or capped pricing reveals whether they truly manage feedstock risk or simply pass it through. Sourcing strategies that survive disruption rely on more than one qualified source, but that does not mean chasing spot lots. Qualify a second or third producer during stable periods, hold buffer inventory at the right point in your network, and build contract terms that allow volume flexibility without penalty. That combination keeps production running when others are renegotiating at the worst possible time.
Contact Us
Contact Person: WANG SIHAI
Email: [email protected]
Tel/WhatsApp: +86-13815295628
Website: https://www.fortunechemtech.com/index_en.html