Full Automatic Underpad Making Machine: Key Advantages for High-Volume Production
2026-10-27
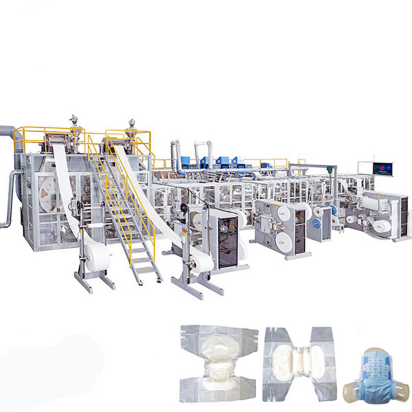
In high-volume production, every second and every gram of material counts. The full automatic underpad making machine has become a game-changer for manufacturers aiming to boost efficiency without compromising quality. But not all machines are built equal. From precision cutting to zero-waste material handling, Womeng brings key advantages that redefine what true automation should deliver. Here’s why forward-thinking factories are making the switch.
When Faster Lines Need Tighter Control
Speeding up a production line often sounds like a straightforward win—more units per hour, better utilization of equipment, and a faster response to market demand. But as throughput climbs, the margin for error shrinks dramatically. Processes that were once forgiving at lower speeds become highly sensitive to tiny variations in temperature, pressure, alignment, or material consistency. A conveyor moving twice as fast leaves less time for inspection and correction, which means a small drift in a cutting blade or a slight viscosity change in a coating fluid can quickly produce hundreds of defective parts before anyone notices. This is where tighter control stops being an optional upgrade and becomes a prerequisite for maintaining yield and quality.
Consider high-speed bottling lines in the beverage industry. At 1,200 bottles per minute, a fill-level sensor has roughly 50 milliseconds to measure and adjust each container. If the control loop lags even slightly, you get underfilled or overfilled bottles—either a compliance issue or product giveaway. Similarly, in semiconductor lithography, as wafer stages accelerate to boost throughput, the overlay accuracy between layers must be held to nanometer tolerances. Older PID controllers tuned for slower operation begin to oscillate or overshoot under these conditions. So engineers turn to model predictive control, feedforward compensation, and high-frequency servo loops that anticipate disturbances rather than merely react to them.
Tighter control at higher speeds also demands better data infrastructure. You can’t rely on periodic sampling or batch-level quality checks; the process needs continuous, real-time feedback from multiple sensors—vibration, thermal imaging, laser micrometers, or in-line spectroscopy. These streams feed into edge computing nodes that adjust actuators within milliseconds. In many cases, the real bottleneck isn’t the mechanical speed but the control system’s ability to keep up. Teams that invest in closed-loop automation and adaptive algorithms find that they can push lines faster while actually reducing scrap rates, because the system constantly self-corrects. The alternative—running fast with loose control—usually ends with a mountain of rework and a very expensive lesson in process dynamics.
Cutting Steps Without Cutting Corners
Trimming a process often gets reduced to a single question: what can we skip? But the sharper question is what actually moves the work forward. Before eliminating any step, trace how it affects the final output. A repetitive approval may feel like overhead, yet it could be the only thing catching errors before they reach a client. The goal is not to make the workflow shorter on paper, but to remove friction while keeping the safeguards that preserve quality.
The people doing the work usually know where the waste hides. Ask them which forms are filled out and never read, which handoffs cause the most waiting, and which checks are purely ceremonial. Replacing one of those with a clear automated log or a shared record can cut hours without lowering standards. When teams help design the change, they are less likely to resent the new process and more likely to flag real risks early.
Set a short list of non-negotiables before you start subtracting. Safety checks, compliance reviews, and data validation steps should remain unless there is a proven equivalent. Once that boundary is clear, you can streamline the rest with confidence. Review the results after a few cycles—delivery speed should improve, but not at the cost of rework or broken trust.
Why High Output Doesn't Have to Mean High Waste
A common assumption is that producing more inevitably creates more scrap, emissions, and discarded resources. Yet many operations now prove the opposite by treating waste as a design failure rather than a byproduct. When output rises through tighter tolerances, smarter scheduling, and better raw material selection, the ratio of waste to finished goods often drops.
The real driver of waste is not volume but variability. Fluctuations in temperature, moisture, or operator technique lead to rejects that get thrown away long before the final product reaches a customer. By stabilizing processes and using real-time monitoring to catch deviations early, high-output lines can maintain consistent quality without generating extra offcuts or defective batches.
Some facilities go further by rethinking what counts as waste. Heat from one stage preheats another, trimmed edges return to the feedstock, and packaging is designed for reuse rather than single trips. These moves don't slow down production; they redirect resources that would otherwise leave as landfill or incinerator ash. The result is a system where higher throughput feeds a tighter resource loop, not a growing waste pile.
Less Downtime, More Pads Per Shift
Frequent stoppages eat away at a shift before anyone notices. The real cost isn't just a paused line; it's the material that cools, the sensors that need recalibration, and the operator who has to walk the whole machine to find the fault. When a pad press stops cleanly only for genuine maintenance, the rhythm of production stops being interrupted by false alarms and starts stacking completed trays.
Smart changeover design keeps the next roll of film ready to splice while the current one is still running, so the transition happens in seconds rather than minutes. Operators stop treating every shift as a battle against the clock and start trusting the machine to hold its pace. That trust shows up in the count at the end of the day: more finished pads, fewer half-formed ones in the scrap bin.
Reliability isn't a feature on a spec sheet. It's the absence of the small, recurring problems that force a line to crawl. When sensors stay aligned and heating zones hold their temperature, the only reason to touch the controls is to make a fine adjustment, not to recover from a fault. That is when a shift produces what it was actually designed to produce.
Keeping Seals Strong When the Line Never Stops
A production line that runs around the clock puts relentless stress on every seal in the system. Heat from constant friction, aggressive cleaning chemicals, and the sheer repetition of pressure cycles slowly eat away at rubber and polymer components. Many seals fail not from a single catastrophic event, but from tiny material fatigues that accumulate day after day until a leak appears. The trick isn't just picking a tough material off the shelf—it's understanding exactly how your specific process wears down a seal over months of nonstop operation.
Material selection becomes the first line of defence. Standard nitrile or EPDM seals often crumble under combined chemical attack and thermal cycling, so moving to perfluoroelastomers or custom-blended polyurethanes can triple service life without a single line stoppage. Equally important is seal geometry: a slightly thicker lip, a better-designed groove, or a self-lubricating surface can disperse stress rather than concentrate it at one weak point. Even something as simple as changing the seal's cross-section from an O-ring to a quad-ring reduces rolling and twisting during high-speed reciprocation, keeping the sealing face intact longer.
Yet even the best seal degrades if the surrounding equipment drifts out of tolerance. Shaft runout, bearing wear, or misaligned flanges create uneven pressure that no seal can resist forever. Routine checks with thermal imaging or ultrasonic leak detectors spot early warning signs—hot spots, tiny gas escapes, or vibration changes—without shutting down the line. Swapping in a replacement seal during a scheduled tool change or brief pause becomes far cheaper than an emergency shutdown after a blowout. In a truly continuous operation, strength isn't just a property of the seal itself; it's a system-level habit of anticipating wear before it turns into downtime.
From Raw Roll to Finished Pad Without the Bottleneck
The moment a raw roll enters the facility, the clock starts ticking. Most lines stall between slitting and lamination because the material waits for downstream equipment to catch up. Here, the roll moves through a continuous flow: unwinding, coating, curing, and die-cutting happen in one coordinated sequence, not as disconnected steps. Operators set the pace by watching tension and temperature in real time, adjusting on the fly rather than stopping for batch changeovers.
What typically creates the bottleneck is the drying stage—adhesive or silicone needs time to set, and conventional ovens force the whole line to slow down. The solution isn't a bigger oven; it's a smarter curing zone that applies targeted heat only where the coating is thickest. This keeps the web moving at a steady speed while the chemistry does its work. As a result, a roll that took six hours to convert now clears the line in under three, with fewer rejects from uneven curing.
The payoff shows up at the die-cutting station. Instead of feeding pre-laminated sheets from a separate batch, the in-line cutter receives a continuous strip with consistent adhesive distribution. Waste drops because there's no misalignment from re-registering between processes. The finished pads come off cleanly, stacked and sealed, ready to ship without ever sitting in a staging area. That's what removing the bottleneck actually looks like—not just faster throughput, but a process where every roll reaches its end form without waiting for permission.
FAQ
The main edge comes from continuous material feeding, synchronized cutting, and automatic stacking. Operators don't need to pause for manual alignment or switching, so the line can sustain 200 to 300 cycles per minute depending on pad size. Fewer touchpoints mean fewer chances for slowdowns or human error.
Sensors track web tension and edge position in real time, so the machine adjusts before misalignment turns into rejects. Automatic splicing on some models also means the line doesn't have to stop for roll changes, avoiding scrap from restarting.
Yes, because the main tasks shift to monitoring touchscreen alarms and keeping raw materials loaded. With automatic counting, stacking, and reject diversion, one person can typically oversee two or three lines, depending on the layout and the machine's self-diagnostic capabilities.
Look for sealed bearings, quick-release folding plates, and a centralized lubrication system. These let technicians perform routine checks and replacements without full disassembly. Modular frame sections also help because a worn cutting or sealing module can be swapped out while the rest of the line keeps moving in some configurations.
Servo motors allow the machine to adjust the cut length and fold position on the fly, compensating for slight variations in material thickness or stretch. This keeps each pad within a tighter tolerance band than clutch or cam systems, which is critical when downstream packaging relies on uniform stacks.
It usually falls between 12 and 24 months for a line running close to capacity. The calculation depends on labor savings, reduced scrap, fewer rejected batches, and the ability to take on larger orders without adding shifts. Many producers also factor in lower training time because the HMI guides operators through changeovers.
Most fully automatic machines accept changeover sets that adjust cutting length, folding width, and stacking height. High-end models store recipes for ten or more pad sizes, so operators can switch from a 60x60 cm pad to a 90x60 cm version in under ten minutes without tools.
Vision sensors or optical detectors catch missing glue lines, off-center cores, or torn nonwoven before the pad reaches the stacker. The system then either flags the stack or diverts it automatically, so the final count per bag matches the label and customers don't receive underweight packs.
Conclusion
High-volume production of underpads demands more than just speed; it requires a machine that stays disciplined when the line accelerates. The full automatic underpad making machine handles faster lines with tighter control, synchronizing every stage so that raw rolls transform into finished pads without a single bottleneck. It cuts steps without cutting corners, streamlining workflows while preserving the structural integrity of each pad. This balance means high output doesn't automatically turn into high waste—precision material handling and smart scrap recovery keep waste fractions remarkably low, even at peak speeds.
Downtime is the silent killer of shift targets, and this machine is engineered to minimize it. Quick-change modules and self-monitoring systems reduce stoppages, translating directly into more pads per shift. Sealing remains robust when the line never stops, with heat and pressure controls that adapt in real time to maintain bond strength across every inch of material. The result is a continuous, reliable flow from raw roll to finished pad—no interruptions, no weak links—making the full automatic underpad making machine a genuine advantage for manufacturers chasing volume without sacrificing quality or yield.
Contact Us
Contact Person: Jessie Lai
Email: [email protected]
Tel/WhatsApp: 86-188594442931
Website: https://www.wm-machinery.com