Custom Plastic Sheet Machine: Key Features to Evaluate Before Making a Purchase
2026-10-28
How many buyers regret their plastic sheet machine within the first six months? The number is higher than you'd think—and it's rarely about the price. The real culprit? Skipping the critical details during evaluation. From roller alignment to extrusion consistency, each specification determines whether your line runs flawlessly or stalls every shift. If you're serious about avoiding that fate, look closely at machines like those from COMRISE, where every feature is engineered with long-term performance in mind. But before you commit to any supplier, here are the key features you absolutely must check.
What Your Raw Materials Actually Demand
Your raw materials are not passive inputs waiting for your process. They come with hard physical and chemical thresholds—humidity limits, temperature bands, shelf-life clocks, and tolerance for vibration. A load of resin left in a hot container doesn't just get warm; it cross-links early and becomes scrap before you ever open the bag. Fresh produce won't forgive a broken cold chain for even two hours. Treat these demands as non-negotiable design constraints, not afterthoughts in a warehouse manual.
Beyond storage conditions, raw materials demand consistency in their own identity. A batch of 316 stainless with a subtle shift in molybdenum content machines differently and fails corrosion tests months later. A spice blend with uneven particle size won't extract flavor the same way in a large-scale kettle. That means your suppliers need to show you process capability data, lot-to-lot variance charts, and real-time batch records—not just a certificate of analysis they printed from a template. Your materials are, in effect, demanding statistical proof that they are what they claim to be, every single delivery.
Finally, raw materials demand a clean paper trail. A mineral sourced from an unverified mine, a timber shipment without chain-of-custody documentation, or a recycled polymer with unknown post-consumer content all carry hidden liabilities. These materials don't announce their problematic origins; they sit quietly in inventory until an audit or a customer question exposes the gap. By then, the cost of tracing back is far higher than the price of a transparent supplier. Your raw materials are asking for proof of origin, ethical extraction, and regulatory compliance—long before they become part of your finished product.
Screw and Barrel Design That Handles the Heat
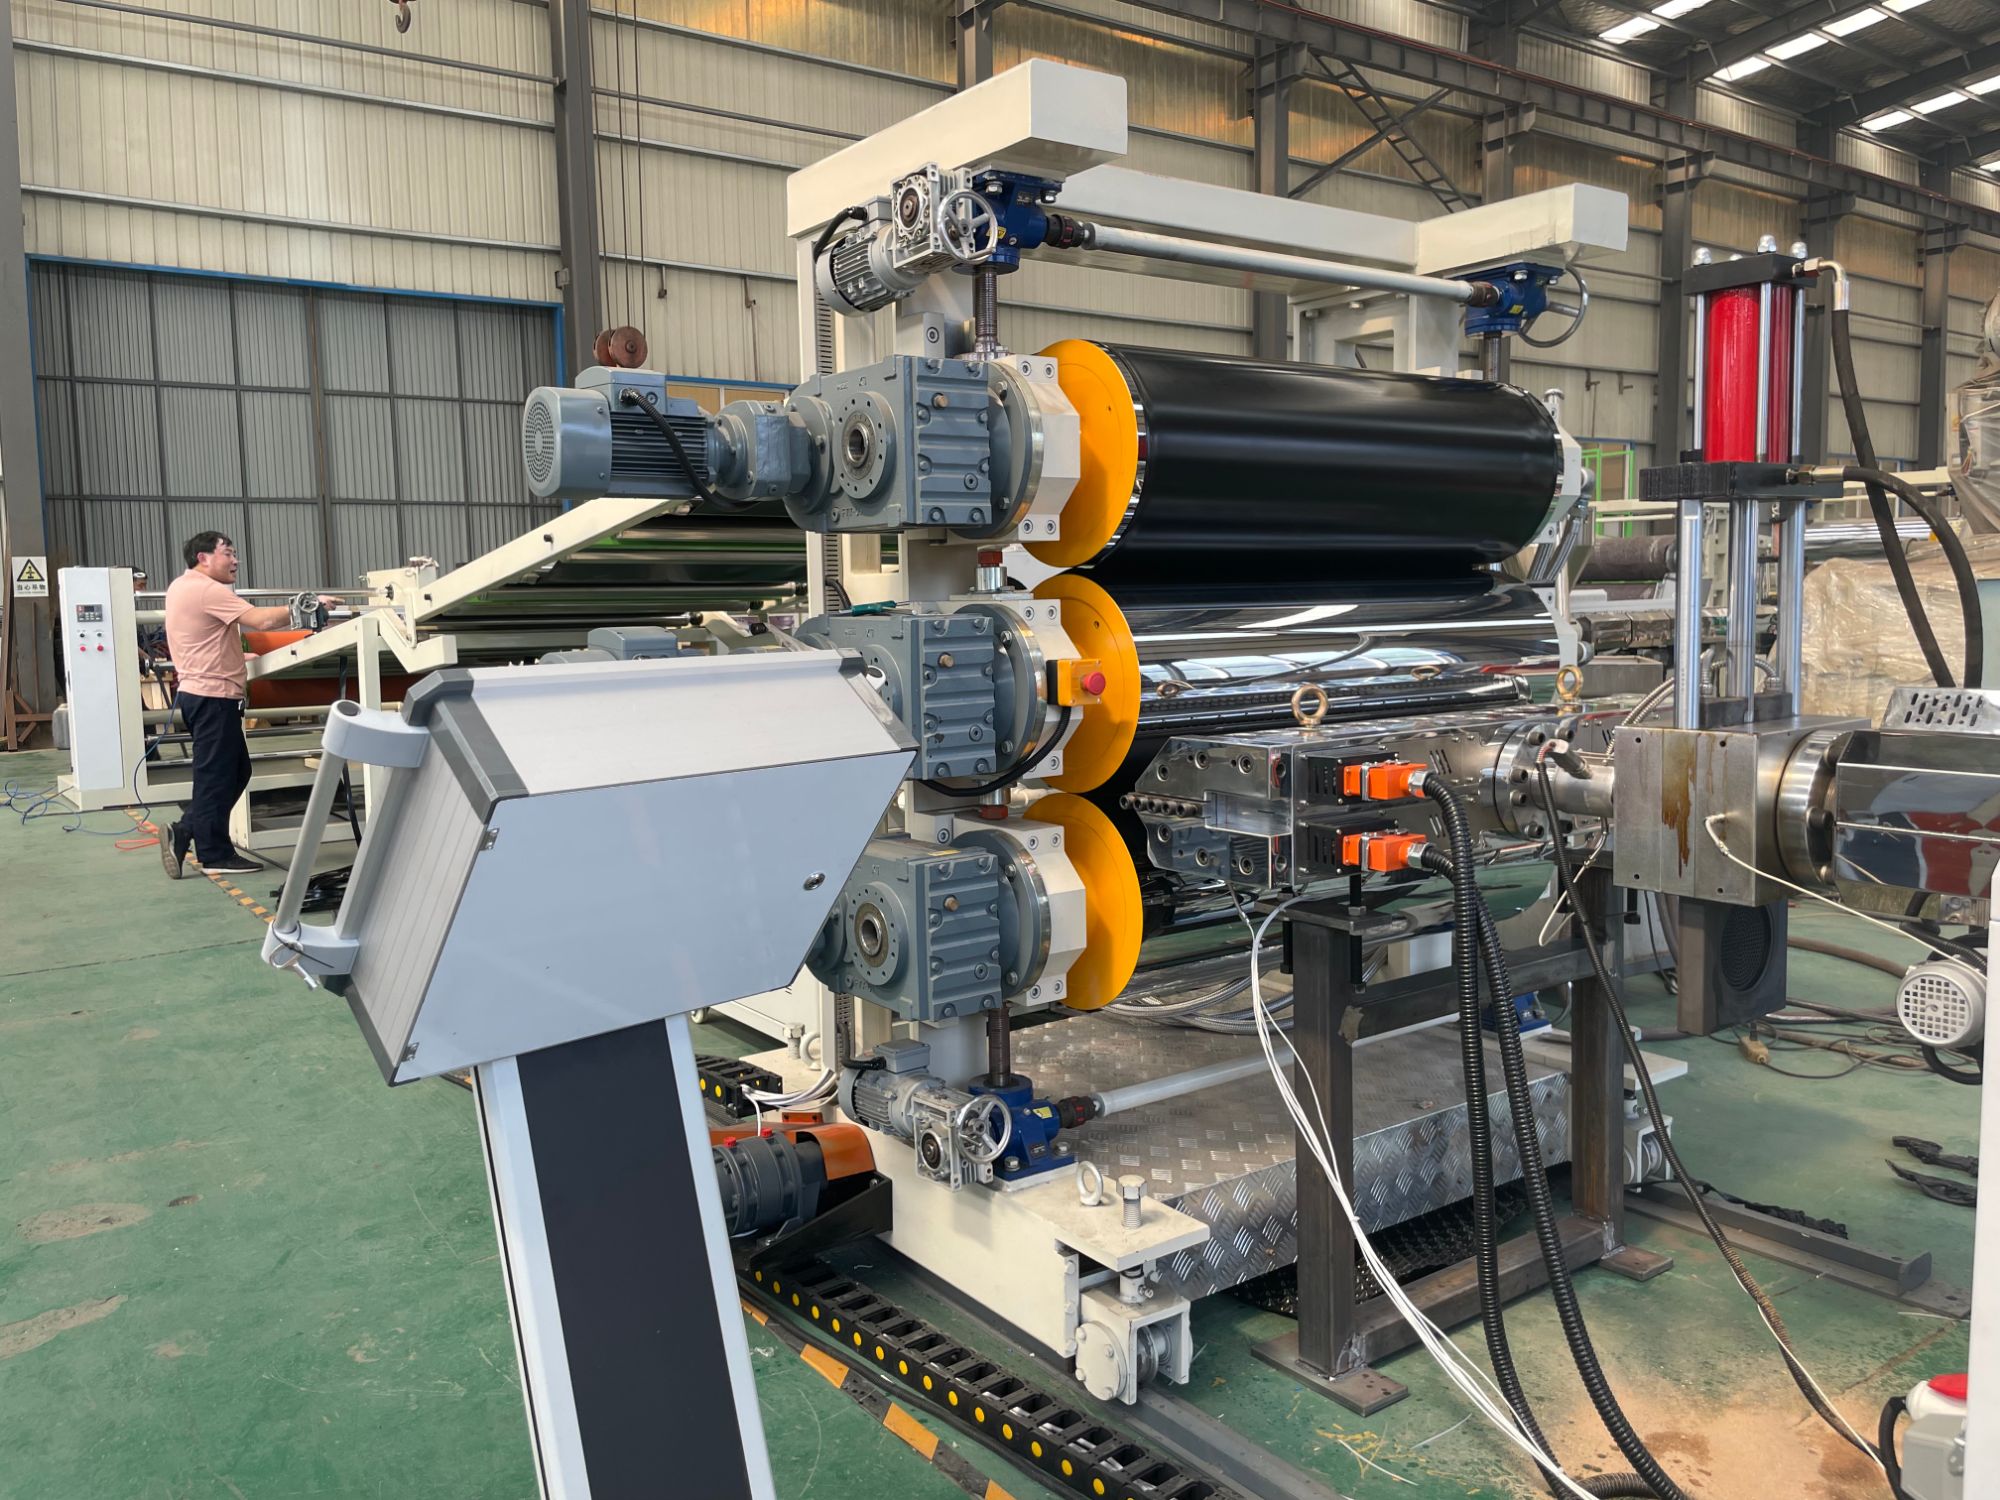
Thermal load is the silent killer of extrusion hardware. When melt temperatures climb, standard screws and barrels expand unevenly, causing wear patterns that look like early fatigue but are actually stress fractures from differential expansion. A heat-ready design accounts for this by matching the coefficient of thermal expansion between the screw core and barrel liner, often using bimetallic alloys or a hardened surface layer that keeps clearance stable from cold start to full throughput.
Barrel cooling channels are usually placed near the feed throat, but for high-heat processes the critical zone shifts to the compression and metering sections. Moving cooling capacity there prevents localized overheating that can degrade polymer and plate out on the screw root. Some designs use spiral-cut channels instead of straight bores, which improves heat transfer uniformity without weakening the barrel wall.
Screw geometry also reacts to heat. Deep screw channels improve plasticizing, but too much depth reduces shear and can leave unmelted particles in a high-temperature melt. A balanced design uses a moderate compression ratio with a longer barrier section, so the screw doesn't rely on brute shear to melt. That keeps melt temperature lower while maintaining output, which extends screw life and avoids thermal breakdown of temperature-sensitive resins.
Thickness Tolerances That Won’t Cause Rework
Setting thickness tolerances too tight is the fastest way to create scrap. A workable range starts with the actual capability of your forming, machining, or coating process, not with a number pulled from a generic chart. For sheet metal, a tolerance of ±0.1 mm on material thickness often sits inside what mills deliver, but once you add bending or welding, local thinning near corners can push you past that limit. Instead, measure the as-built thickness at the section you care about, not the nominal stock size. If your inspection data shows a spread of 0.08 mm across a batch, a ±0.05 mm spec will guarantee rework; a ±0.15 mm spec will pass nearly every good part while still catching real defects.
The key is to tie the tolerance to function, not to habit. A sealing face may need thickness held within 0.02 mm because a step there causes leaks, but the same part’s web or flange can usually tolerate three to five times that variation without any performance change. Write separate callouts for those zones instead of applying one blanket tolerance to the whole drawing. This makes the design look messier, but it eliminates arguments on the shop floor and prevents machinists from overworking non-critical surfaces to meet an unnecessary number.
Also consider what your measurement method can actually resolve. A micrometer reads differently than a laser scanner or a CMM, and if your spec is smaller than the gauge’s repeatability, you’ll reject good parts based on noise. Match the tolerance to the instrument’s uncertainty, and add a note about which measurement protocol defines compliance. When everyone checks thickness the same way, the number of borderline parts that get sent back for rework drops sharply.
Line Speed vs. Quality: Where’s the Trade-Off?
Many manufacturers assume that cranking up line speed automatically erodes quality, but the relationship is rarely that clean. In reality, the trade-off lives in specific failure points—weld spatter, uneven adhesive beads, misaligned labels—that only appear once a process moves past a certain cadence. Below that threshold, quality can hold steady or even improve because operators and automated inspection systems get more repetitions to fine-tune their timing.
The real cost isn't speed itself; it's the lack of feedback loops at higher rates. A slow line gives inspectors time to catch weak joints or surface flaws before they leave the cell. At speed, those same defects slip through unless you've already built in vision checks, real-time torque monitoring, or go/no-go gauges that react in milliseconds. So the question shifts from "how fast can we go?" to "what can we measure at that speed without slowing down?"
Sometimes the best answer is to deliberately slow a single station, not the whole line, to protect quality where it matters most. For example, letting a curing oven run a few seconds longer per unit can eliminate rework downstream far more cheaply than adding an extra inspection shift. That kind of targeted trade-off—finding the station where a small speed reduction buys the most quality—tends to beat uniform acceleration or blanket slowdowns.
Energy Consumption You Can Budget For
Most appliances either hide their energy appetite or hit you with a bill that feels random. This one takes the opposite approach. The draw is measured, modest, and consistent, so you can tally the cost before you even switch it on. No guessing, no end-of-month regret—just a clear number you can fold into your regular utilities without rearranging your budget.
That predictability changes how you use the unit. Run it a few extra hours on a sticky afternoon. Let it hum through the night when sleep matters more than saving a few cents. Because the consumption stays within a narrow band, those small decisions don't cascade into a bill that wrecks the week.
It's not about being frugal for its own sake. It's about matching your comfort to your actual cost of living, instead of worrying that every degree of cool air is quietly draining your wallet. Once you know the number, you can stop tracking pennies and start using the space the way you intended.
Support After the Invoice Is Paid
Paying an invoice doesn't close the door on our involvement. In fact, that's when the real work often begins. We continue to stand behind every transaction, making sure the product or service you've invested in performs exactly as expected. If something feels off, you don't need to navigate a maze of phone menus or wait through generic ticket queues—just reach out and we'll work through it together.
Beyond fixing problems, we keep an eye on how things are running on your end. That means occasional check-ins, practical tips for getting more out of what you've purchased, and honest advice if we see a better way to use the tools you already have. There's no upsell pressure, just straightforward guidance based on what's actually happening in your day-to-day operations.
As your business shifts, your needs change too. We stay available for those moments—whether it's adjusting settings, explaining a new feature, or simply answering a question that came up weeks after the invoice was settled. This ongoing support isn't a bonus feature; it's part of how we operate, because a paid invoice is just one step in a longer working relationship.
FAQ
Focus on the screw design, temperature control accuracy, and the actual thickness tolerance of the sheet output. Don't just look at the price tag—a cheaper machine can quickly cost more through downtime and scrap rates than the initial savings.
Cooling directly affects sheet flatness and crystallinity, especially for materials like PP or PET. Check the cooling roll diameter, flow channel design, and temperature uniformity. Some manufacturers cut corners in this area, and you will see it in warped or inconsistent sheets.
A truly custom machine should allow screw and die changes to run different resins like ABS, HIPS, PE, or PP. But also ask about changeover time and cleaning difficulty, otherwise the claimed versatility is just a nice-sounding feature that slows you down.
A modern line should offer real-time data logging, recipe storage, and remote diagnostics. If the operator interface is still old-style buttons and analog gauges, fine-tuning the process will be painful and batch consistency will suffer.
At a minimum, you need installation, operator training, and fast spare parts supply. Ask if they have a local service team and whether software upgrades are included. For cross-border purchases, confirm the actual response time, not just a promise.
Look for a die flow channel optimized through simulation for your specific product, and whether closed-loop thickness control with an online gauge is offered. These options cost more upfront but significantly reduce thickness variation and material waste.
Check the heater zoning, motor efficiency rating, and insulation thickness. Some machines show low nominal power but actually consume more energy because fluctuating temperature control forces heaters to cycle frequently. Request measured data from typical operating conditions.
Depending on complexity, expect 3-6 months from design approval to delivery, plus 2-4 weeks for on-site installation and debugging. If a supplier promises much faster, be suspicious that you are getting a modified standard machine rather than a true custom build.
Conclusion
Before committing to a custom plastic sheet machine, start by looking at what your raw materials actually demand. Different polymers, regrind ratios, and additive packages can shift melt behavior drastically, and a screw that works fine for virgin HDPE might struggle once you introduce recycled content or heat-sensitive resins. The screw and barrel design needs to handle the heat without creating dead zones or excessive shear, because that's where burned specks and inconsistent melt quality come from. Thickness tolerances are another area where machines quietly fail: if the die gap and downstream calibration aren't built to hold tight numbers across the full sheet width, you'll end up with edge thinning or center crown, and that means rework, scrap, and lost margin. The right machine should demonstrate repeatable gauge control under realistic production conditions, not just on a clean demo run.
Line speed and quality are usually talked about as a trade-off, but a well-engineered machine pushes that balance further than you'd expect. Higher output only pays off if the sheet stays flat, clear, and within spec at the take-off, so pay attention to roll stack design, cooling capacity, and how the machine handles acceleration and deceleration. Energy consumption is often treated as an afterthought, yet it shows up on every invoice: barrel heaters, drive motors, and vacuum pumps run for thousands of hours, and a poorly optimized barrel insulation or oversized motor can add real cost per kilogram. Finally, look hard at what happens after the invoice is paid. A supplier that offers real startup assistance, spare parts availability, and someone who actually answers the phone when a drive faults at 2 a.m. will save you far more than a slightly lower purchase price.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com