China Aluminum Ice Bucket Factory: What to Look for in Quality and Customization
2026-10-06
If you think all aluminum ice buckets from China are the same, you’ve likely never compared a flimsy single-wall bucket to a double-wall design that keeps ice solid through a summer party. Quality and customization aren’t just buzzwords here—they’re the details that determine whether your order builds brand loyalty or gets quietly retired. APEXAL has spent years inside Chinese factories, and this guide maps out what actually matters when evaluating a supplier.
Read the Spec Sheet Like a Machinist
A machinist reads a spec sheet the way a mechanic listens to an engine: not for the obvious, but for the small noises that predict trouble. Start with the tolerance block and the material line before you even look at the big dimensions. A 0.005-inch tolerance on a milled pocket might sound forgiving, but if the datum scheme leaves it floating from two different edges, you'll chase that number all afternoon.
Notes like 'break all sharp edges' or '32 RMS finish' are not decoration. The 32 tells you the tool has to leave a consistent witness mark, which means your feeds, speeds, and even the machine's way condition matter more than the diameter of the end mill. And when you see a true position callout with an MMC modifier, you better know whether the hole gets a dowel pin or a bolt through it—that changes how much bonus tolerance is actually usable.
Material and hardness notes are the quiet schedule killers. 4140 annealed cuts far differently than 4140 heat-treated to 28-32 HRC; the spec sheet won't tell you that, but a machinist reads the hardness range and automatically adds roughing passes, slows the feed, and checks the insert grade. Same with a note that says 'stress relieve after roughing'—that's not a suggestion, it's a map for when the part will move on you.
Demand Weld Samples from the Actual Production Line
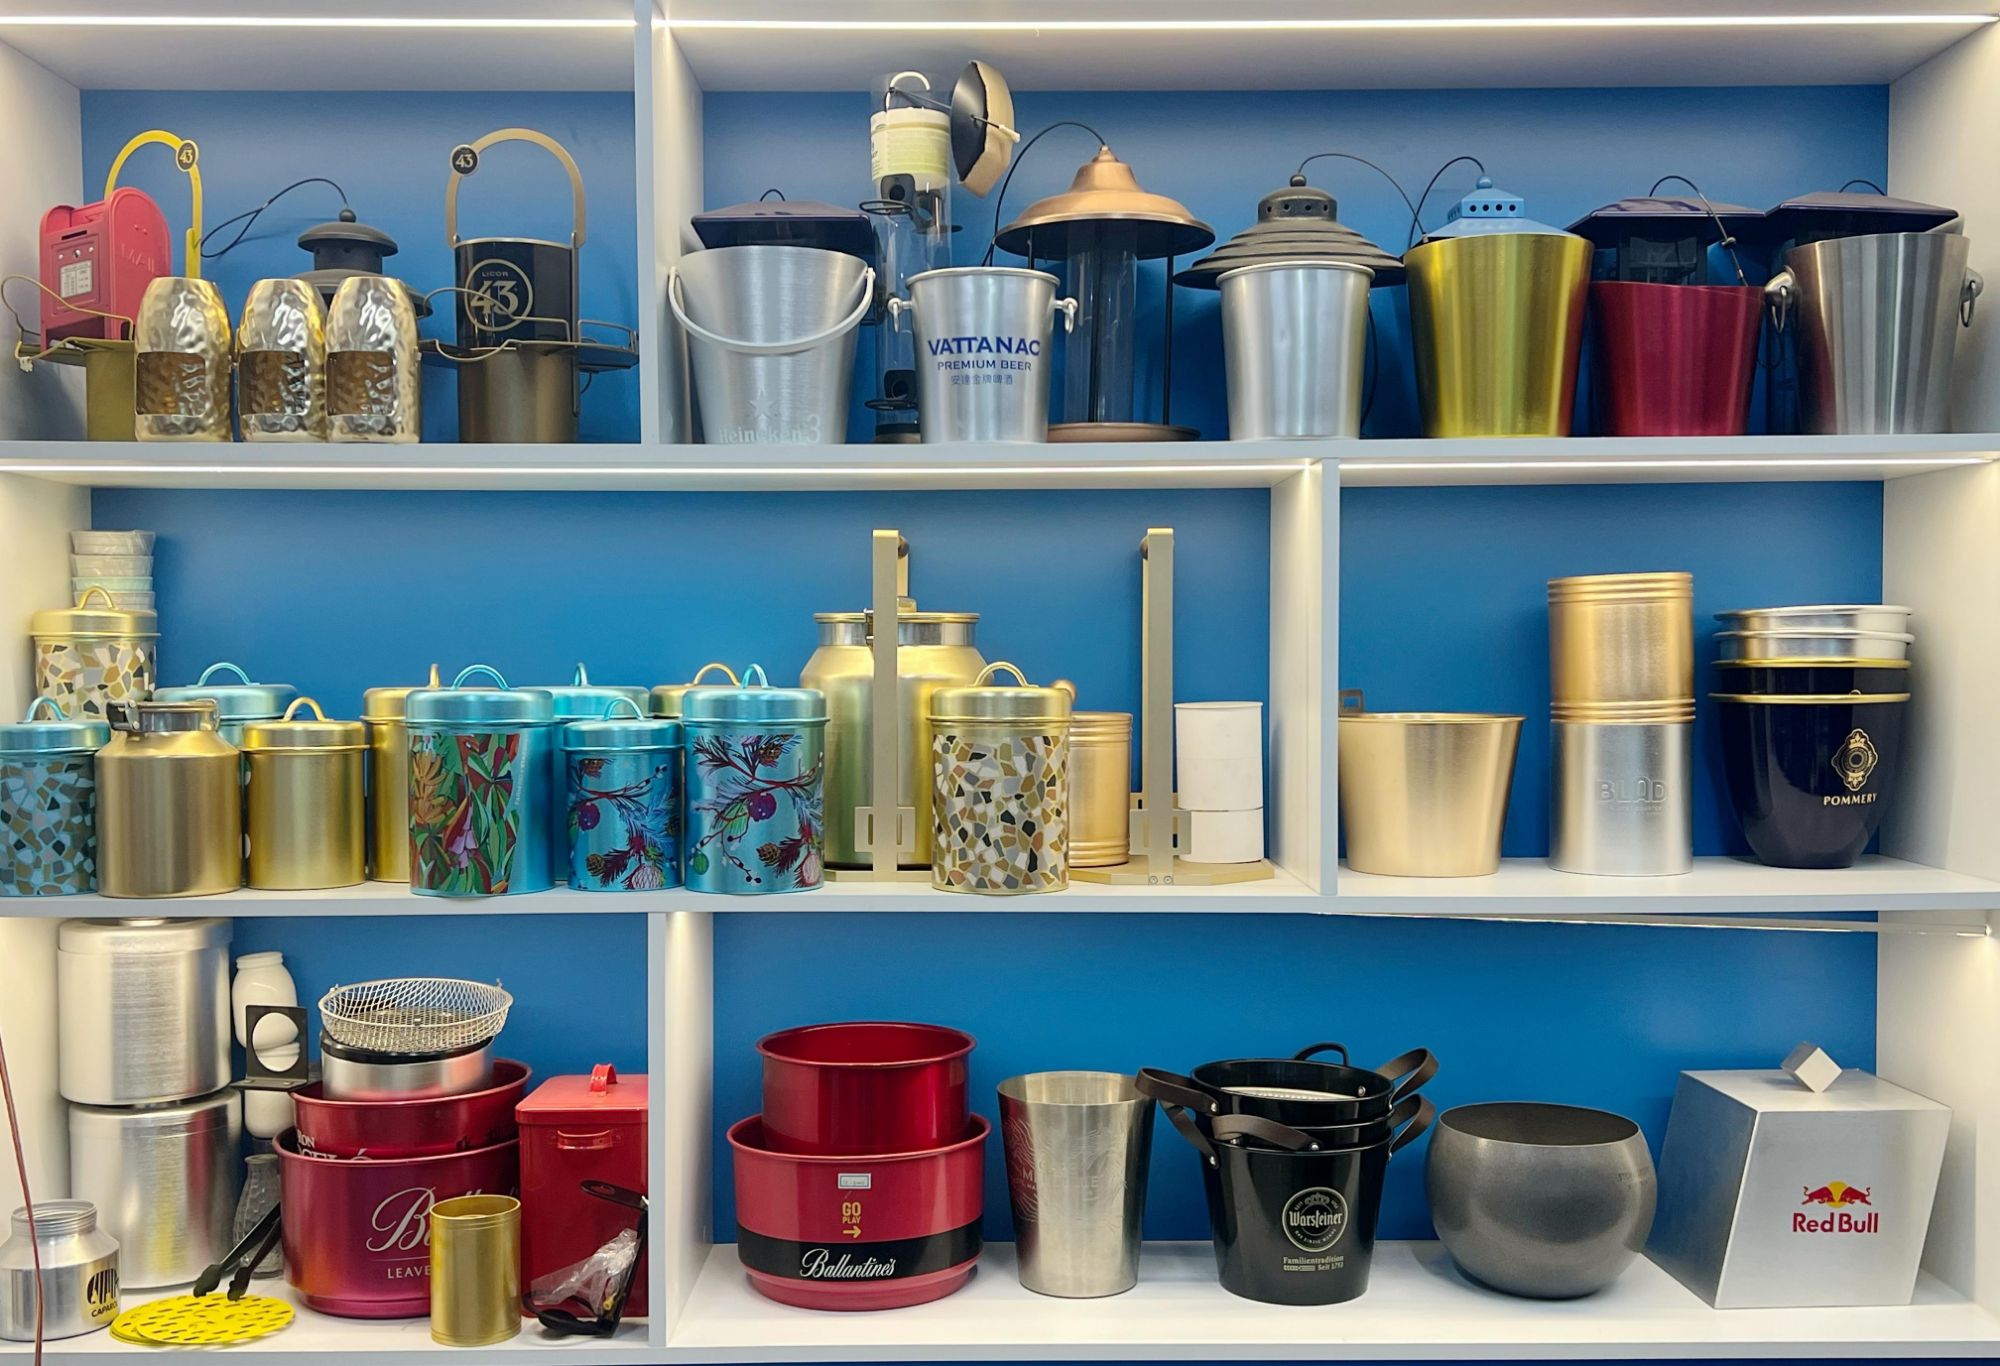
A weld coupon produced in a quiet corner of the lab tells you almost nothing about what happens on a Tuesday afternoon when the line is running at full speed. Real production welds are made with slightly worn fixtures, by operators who may be rushing to meet quota, on material that has sat in the yard or picked up light surface contamination. If your sample doesn't come from that environment, you're not testing your actual process—you're testing an idealized version that will never show up in the field.
To get meaningful data, pull samples directly from the production flow without giving the line advance notice. Pick them at random intervals across different shifts, different operators, and different material batches. Record the exact welding parameters, the operator's name, the time of day, and the fixture or station used. This kind of unannounced sampling prevents the "special effort" effect where everyone suddenly becomes more careful because they know a test piece is being watched.
Then run destructive tests, macro-etches, or hardness traverses on those production samples. Compare the results across shifts and operators, not just against a lab baseline. If the production welds consistently pass, you have a process you can trust. If they don't, you've uncovered a real problem before it turns into field failures or warranty claims. Skipping this step and relying on lab-made samples is how weld quality programs get a false sense of security.
Check the Finish Under Condensation, Not Just in Product Photos
A product photo can hide almost anything if the lighting is soft enough. But run a cold glass across a tabletop or leave a metal fixture in a humid bathroom overnight, and every tiny flaw in the finish surfaces as a dull patch, a bubble, or a streak that no camera angle would ever catch. Condensation acts like a magnifying glass for the topcoat—it clings unevenly wherever the seal is thin or the surface wasn’t prepped properly.
What looks flawless on a screen often falls apart the moment moisture beads on it. Pinholes, micro-cracks, and areas where the coating was applied too lightly become obvious because water gathers there instead of rolling off. If you’re buying anything that will live in a kitchen, bathroom, or covered porch, ignore the marketing shots and ask how the finish behaves with a layer of dew on it.
A quick test beats any spec sheet: breathe on the surface like you’re fogging a mirror, or wipe it with a damp cloth and watch how the water sits. If the finish breaks into flat patches or leaves foggy marks after drying, that’s the real story. The product photos show you the color; condensation shows you the quality.
Push for Custom Shapes and Handles Beyond Standard Molds
Standard molds have their limits, especially when a project calls for a silhouette that doesn't fit the usual catalog. We've seen enough requests for angled grips, asymmetric handles, and sculpted edges to know that off-the-shelf shapes rarely satisfy a specific use case. That's why we moved toward building custom geometries from scratch—whether it's a contoured hand grip for an industrial tool or a low-profile handle that has to sit flush in tight cabinetry.
The real shift happens when you stop thinking of a handle as a separate part and start integrating it with the body. Custom shapes allow for better weight distribution, fewer seams, and a more deliberate tactile feel. Instead of forcing a design to fit an existing cavity, we let the intended hand position and motion drive the mold design. It takes longer up front, but the result feels less like a generic component and more like something made for the task.
Beyond aesthetics, going custom also opens up options for ergonomic testing and rapid iteration with low-volume runs. You're not locked into a one-size-fits-all profile because the tooling was built for someone else's product. That flexibility matters when the difference between a good handle and a great one comes down to a few millimeters of contour or a slightly softer radius near the thumb rest.
Ask How the Lid Seals After Fifty Open-and-Close Cycles
Any lid can feel snug on day one, but the real test comes after repeated use. After fifty open-and-close cycles, a well-designed seal should still press down with the same reassurance as the first time. The gasket needs to retain its shape without flattening or developing micro-tears, and the latch mechanism must stay tight enough to keep air and moisture out. It’s not just about the rubber doing its job—it’s about how the hinge, the rim, and the locking tab all hold up together.
We put the lid through exactly that: fifty full cycles, opening and closing it the way you would in a busy kitchen. By the end, we check for any loosening at the edges or a drop in resistance when you press down. A good lid will still give that faint suction sound when you lift it, and the seal ring won’t show any permanent compression. If it starts to feel wobbly or you can slip a fingernail under the rim without effort, that’s a sign the seal has degraded.
For everyday use, this matters more than you’d think. A lid that seals well after fifty cycles means leftovers stay fresh longer, liquids don’t leak in your bag, and you don’t have to wrestle with a warped edge. It’s the difference between a container that lasts a season and one that lasts for years.
Validate Export Packaging with a Drop Test Video
A quick smartphone clip of a boxed shipment hitting concrete from waist height can settle arguments faster than any spec sheet. Set up the camera at a slight angle so it captures both the impact point and the way flaps or corners buckle. Record in slow motion if your phone allows — the extra frames make it easier to spot whether cushioning shifted before the outer carton even shows a crease.
Run the test with the package oriented in the same way it will travel: label up, on a pallet, or stacked under two other boxes. Toss it once on a corner, once on an edge, and once flat. Compare the footage against your packaging checklist, not just for visible cracks but for sounds that suggest internal movement. If inner boxes slide or inserts compress, that's a fail even if the outer shell looks fine.
Send the video to your freight forwarder or distributor without commentary. A ten-second drop test clip gives them a concrete reference for how your export cartons behave under rough handling, making it easier to push back on damage claims or adjust void fill before a full production run.
FAQ
Look closely at how they handle raw material sourcing and surface finishing. A dependable factory will openly share details about the aluminum grade, thickness tolerances, and the exact anodizing or powder coating process used. If they dodge questions about material specs or only talk about low prices, that is usually a warning sign.
Ask for food-grade certifications or test reports for the interior lining. Many good factories use anodized aluminum or food-safe coatings that prevent metallic taste and corrosion. You can also request a small sample and run a simple smell and stain test at home before committing to a larger order.
Customization goes far beyond a logo. You can often choose the bucket's diameter, height, rim style, handle design, and whether the lid has a silicone seal. Some factories also offer laser engraving, embossed logos, color matching to a Pantone code, and even custom packaging with your brand story.
Thicker walls do two things: they insulate better and they resist dents during shipping and daily use. A flimsy bucket might look fine in photos but arrive with creases. A good factory will specify wall thickness in millimeters for the body, rim, and base, not just give a vague 'premium' label.
Yes, and any factory that refuses a small trial order without a strong reason should be approached with caution. Trial runs let you check the actual finish, packaging, and how the bucket handles ice melt. It is a normal part of building a long-term supplier relationship, not an unreasonable demand.
Anodized finishes tend to resist scratches and corrosion better than plain paint. Powder coating offers more color choices and a tough outer layer. If the bucket will sit in wet conditions often, ask about a clear topcoat or a double-layer coating to slow down wear around the rim and handles.
After sample approval, production typically takes 20 to 40 days depending on order size and finishing complexity. Holiday periods and raw material shortages can stretch that, so it is wise to add a two-week buffer. A factory that promises unusually fast delivery at a low price may be skipping quality checks.
Watch for vague answers about alloy grade, no written quality checklist, inconsistent sample quality between rounds, or pressure to confirm an order before you have tested a sample. Also be wary if the factory cannot explain how they handle defects or what their rejection rate is.
Conclusion
When evaluating a Chinese aluminum ice bucket factory, move past glossy catalogs and start with the engineering details. Ask for the actual spec sheet and read it the way a machinist would—tolerances, material grade, wall thickness, and weld geometry matter more than the listed capacity. Request weld samples pulled directly from the production line, not hand-picked showroom pieces. In humid or outdoor settings, condensation exposes micro-pitting and uneven anodizing that studio photos hide, so check the surface under cold, wet conditions before committing.
Customization shouldn't stop at a logo. Press the factory on non-standard shapes, integrated handles, or reinforced bases that go beyond their existing mold library. The lid is often the weak point: ask how the seal behaves after fifty open-and-close cycles, and whether the gasket retains its compression without warping. Finally, insist on seeing a drop test video for export packaging—not just a certificate. A factory that documents its own packaging failures and fixes them is one you can actually trust with large orders.
Contact Us
Contact Person: Milo
Email: [email protected]
Tel/WhatsApp: +86 18621923991
Website: https://www.dgbaide.com